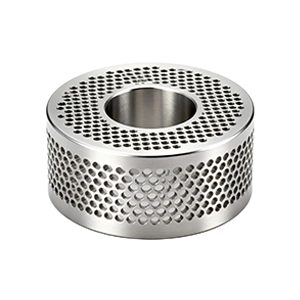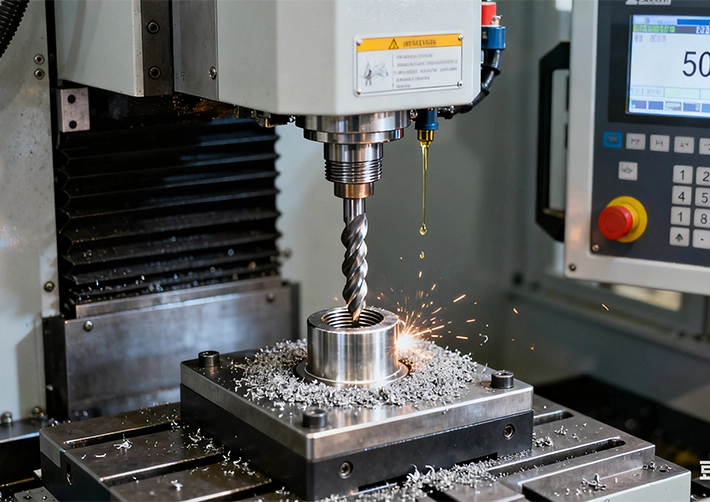
3, 4, 5-Axis CNC Milling
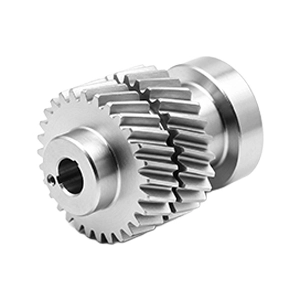
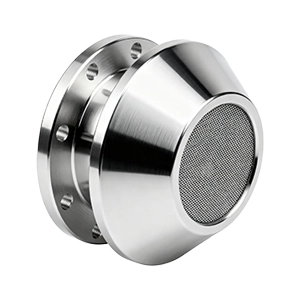
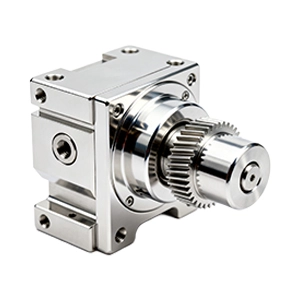
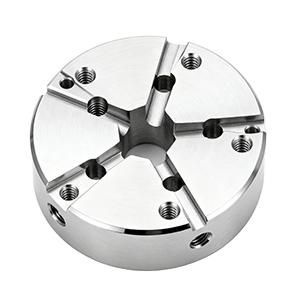
Multi-axis milling for stainless steels (304/316/17-4/410). Rigid setups, coolant-through tooling and balanced parameters deliver tight tolerances, clean edges, and stable dimensions even on thin walls or complex geometry.

High-Precision Machining for Durable Stainless Steel Parts
Custom Prototypes & Production with 3-Axis, 4-Axis, and 5-Axis CNC
| Feature | Detail |
|---|---|
| Max Part Size (X/Y/Z) | 2300 × 1500 × 600 mm |
| Minimum Feature Size | ⌀1 mm |
| Wall Thickness | 0.25 mm |
| Tolerance | ±0.005 mm |
| Surface Finish (as milled) | Ra 0.4–3.2 µm |
| Standard Lead Time | 3 working-days for rapid prototyping |
| Pricing Level | To be confirmed after design review |
| Type of Machine | Gantry CNC / 3-4-5-Axis CNC / Mill-Turn Compound CNC / Swiss-Type CNC / Turning Machine...etc... |
| Stainless Grades | 304 / 304L, 316 / 316L, 17-4 PH, 410 / 416 |
Multi-axis milling for stainless steels (304/316/17-4/410). Rigid setups, coolant-through tooling and balanced parameters deliver tight tolerances, clean edges, and stable dimensions even on thin walls or complex geometry.
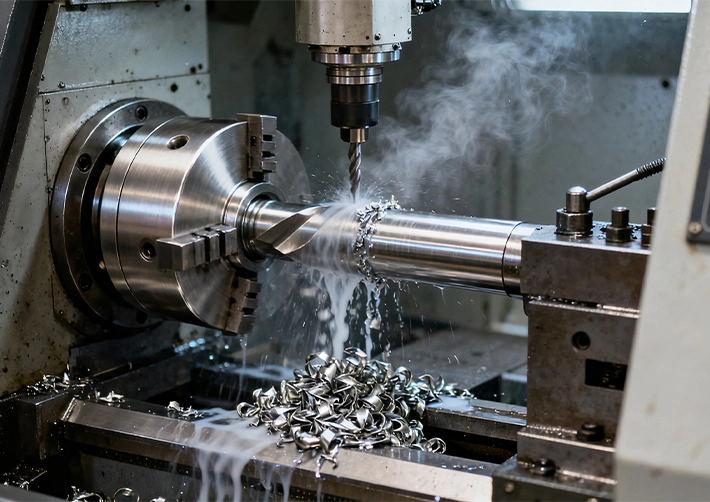
From small bushings to long shafts, we turn stainless with steady chip flow and smooth finishes. Mill-turn consolidation cuts setups and lead time while improving concentricity and overall quality.
| Feature | Detail |
|---|---|
| Max Part Size (X/Y/Z) | 2300 × 1500 × 600 mm |
| Minimum Feature Size | ⌀1 mm |
| Wall Thickness | 0.25 mm |
| Tolerance | ±0.005 mm |
| Surface Finish (as milled) | Ra 0.4–3.2 µm |
| Standard Lead Time | 3 working-days for rapid prototyping |
| Pricing Level | To be confirmed after design review |
| Type of Machine | Gantry CNC / 3-4-5-Axis CNC / Mill-Turn Compound CNC / Swiss-Type CNC / Turning Machine...etc... |
| Stainless Grades | 304 / 304L, 316 / 316L, 17-4 PH, 410 / 416 |
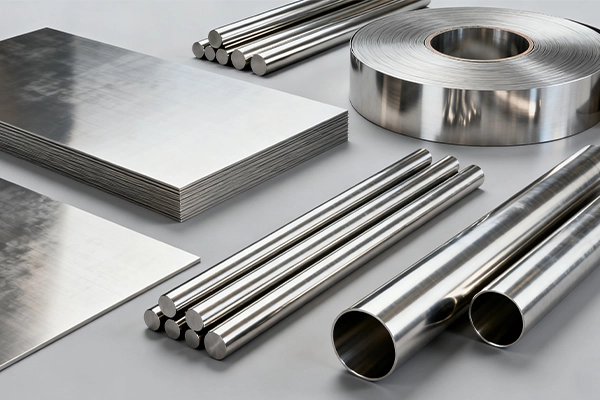
We stock popular grades for prototypes and production. Need a special spec? Contact us.
Use sharp carbide, adequate coolant, and avoid rubbing to maintain a clean finish.
Apply high-pressure coolant and conservative SFM for consistent surface quality.
Use rigid setups, constant feed; consider age-hardening after rough/finish sequence.
Great on lathes; use proper edge prep and coolant for burr control and finish.