Tool Steel Machining Services

Precision Machining for High-Strength Tool Steel Components
Custom Prototypes & Production with Advanced CNC Capabilities

What is Tool Steel CNC Machining?

Tool steel CNC machining focuses on high-carbon and alloy steels engineered for wear resistance, hardness, and toughness. Typical grades include O1/A2/D2 for cold work, H13 for hot work, S7 for shock resistance, and P20 for mold bases.

  • Tooling: Fine-grain carbide, tough coatings (TiAlN/TiCN) to handle abrasion and heat.
  • Coolant: Flood or high-pressure coolant; through-tool preferred for deep features.
  • Feeds/Speeds: Maintain chip load—avoid rubbing to limit work-hardening and edge chipping.
  • Rigidity: Rigid fixturing + short stick-out = better surface and dimensional control.
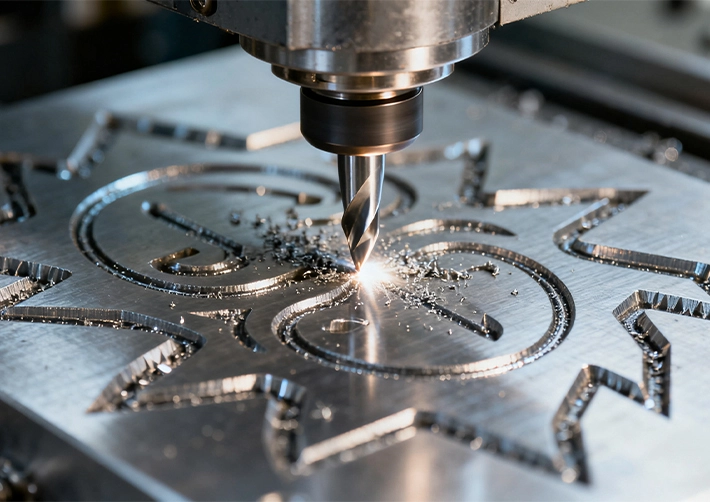
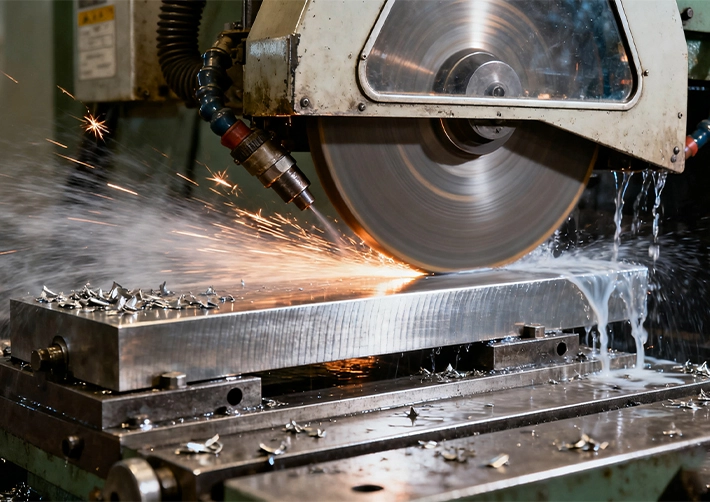
Tool steel CNC machining overview with carbide end mill and flood coolant
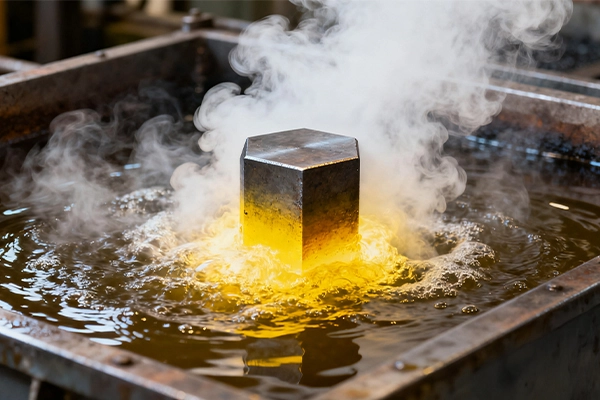
Tool steel heat-treatment stages: annealed, pre-hardened, hardened & tempered

Why Tool Steel Is Challenging?

High hardness and abrasion resistance make chip formation tougher—tools wear fast and heat builds quickly. Picking the right condition matters: annealed for roughing/forming, pre-hardened for bases, hardened & tempered for long-life tooling.

For best stability: rough in soft/annealed state → stress-relieve → harden/temper → finish by hard-milling, grinding, or EDM.

Precision Tool Steel CNC Machining

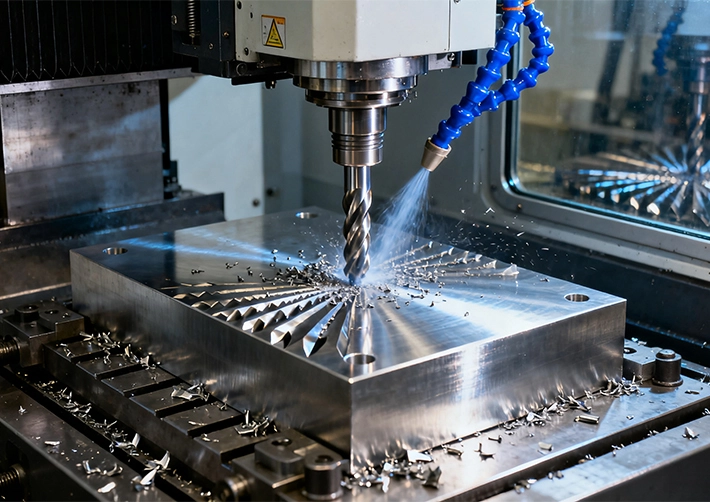
Tool steel 3,4,5-axis CNC milling with through-tool coolant

3, 4, 5-Axis CNC Milling

Multi-axis machining for complex cavities, ribs, and hard-milling. Rigid setups, balanced holders, and coated carbide deliver clean walls and consistent geometry in both annealed and hardened tool steels.

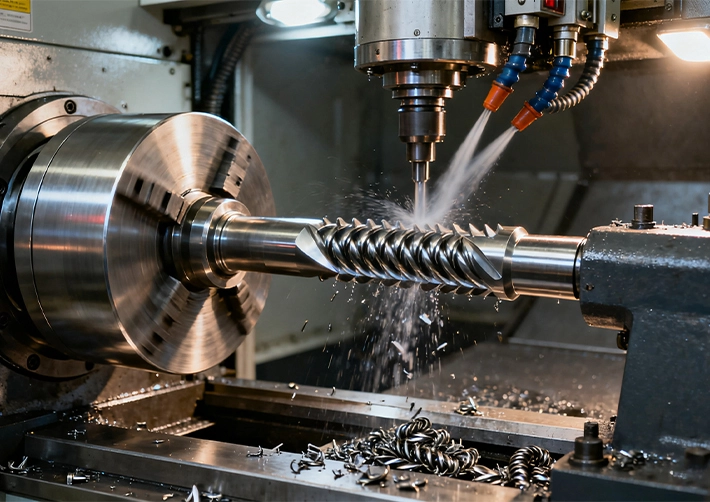
Tool steel CNC turning and mill-turn of shafts and cores

CNC Turning & Mill-Turn

From punches and sleeves to core pins and shafts, combined turning + milling in one setup improves concentricity, finish, and lead time—ideal for prototype to production.

Tool Steel CNC Machining Capabilities

FeatureDetail
Max Part Size (X/Y/Z)2300 × 1500 × 600 mm
Minimum Feature Size⌀1 mm
Wall Thickness0.25 mm
Tolerance±0.005 mm
Surface Finish (as milled)Ra 0.4–3.2 µm
Standard Lead Time3 working-days for rapid prototyping
Pricing LevelTo be confirmed after design review
Type of MachineGantry CNC / 3-4-5-Axis CNC / Mill-Turn Compound CNC / Swiss-Type CNC / Turning Machine...etc...
Tool Steel GradesO1 (Oil-Hardening), A2 (Air-Hardening), D2 (High-Carbon/High-Chromium), H13 (Hot-Work)

Tool Steel Grades

Common grades for cold work, hot work, shock-resistant, and mold tooling. Need a specific spec? Contact us.

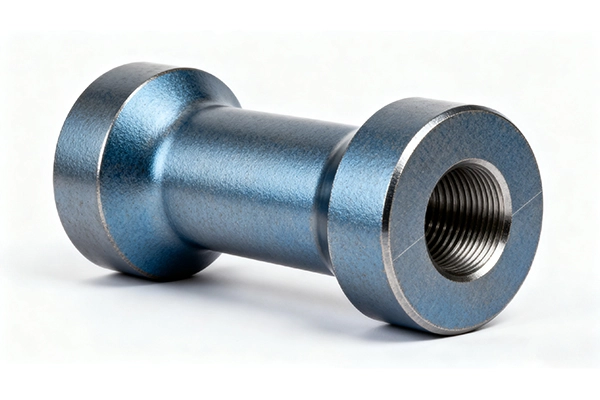
O1 tool steel machined blank (3:2)

O1 (Oil-Hardening)

  • Good wear resistance; fine detail capability
  • Machines well in annealed state
  • Harden in oil; temper for target HRC
  • General punches, dies, fixtures

Rough/slot in annealed → heat treat → finish mill/grind for final fit.

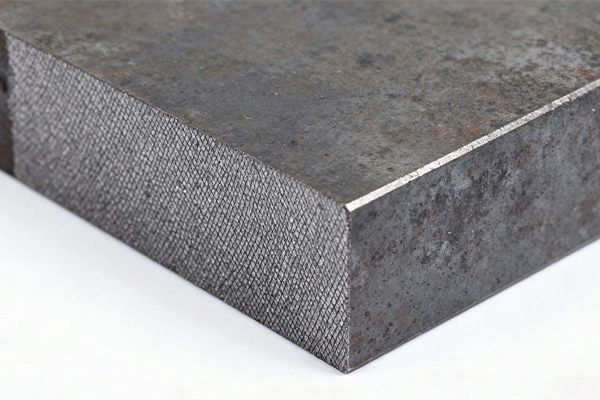
A2 tool steel machined plate (3:2)

A2 (Air-Hardening)

  • Balanced wear/toughness; stable on heat treat
  • Hard-milling feasible; low distortion
  • Cold-work dies, form tools, gauges
  • Common shop standard grade

Air-hardening minimizes distortion—great for tight-tolerance tools after HT.

D2 tool steel machined insert (3:2)

D2 (High-Carbon/High-Chromium)

  • Very high wear resistance; abrasion-intense cuts
  • Harder to machine—use coated carbide
  • Blanking dies, wear inserts, shear blades
  • Consider EDM/grinding for finish

Plan for lower SFM, aggressive coolant, and rigid workholding to protect edges.

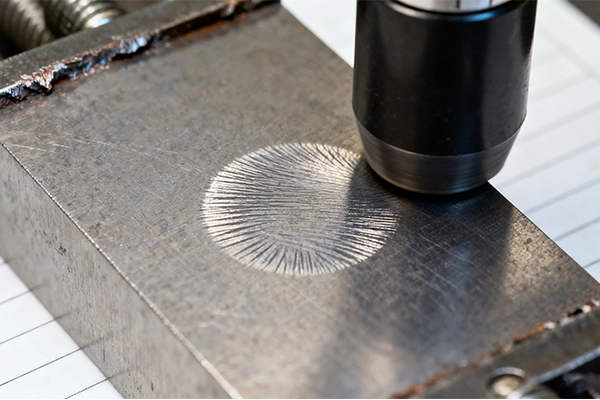
H13 hot-work tool steel mold core (3:2)

H13 (Hot-Work)

  • High hot-strength; thermal fatigue resistance
  • Die-casting dies, hot runners, cores
  • Pre-hard & hardened options
  • Finish via hard-milling, EDM, polish

Use through-coolant and stable holders; step down to control heat and burrs.

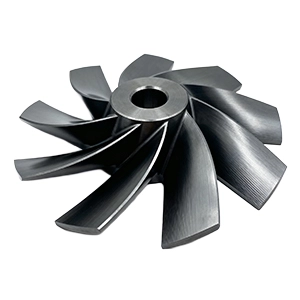
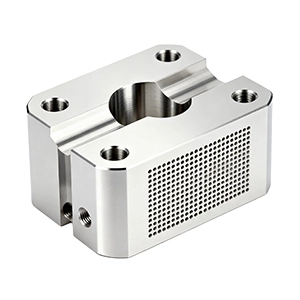
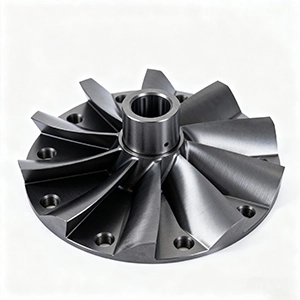
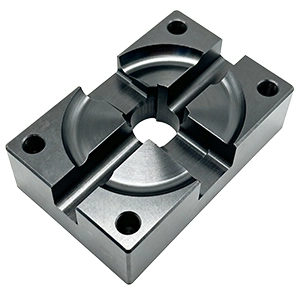
Display of Our CNC Machining Tool Steel Parts

Request A Quote
Upload your drawing and get a quote within 24 hours.