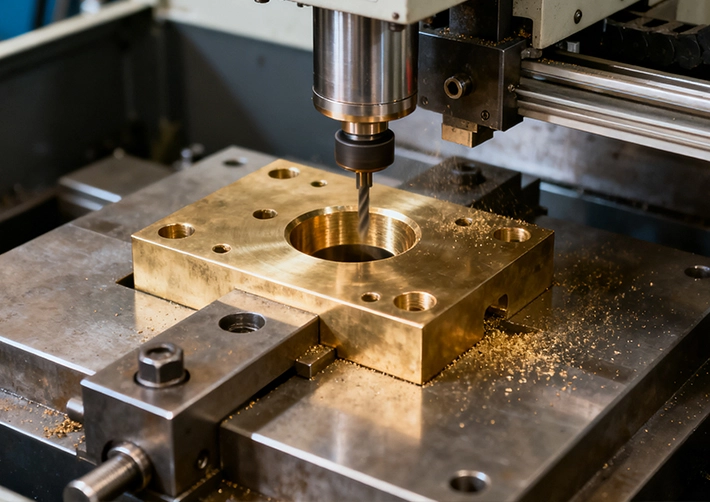
3, 4, 5-Axis CNC Milling
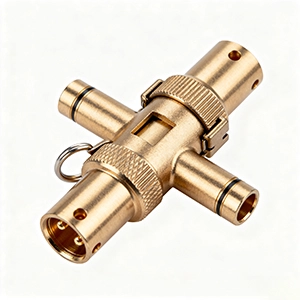
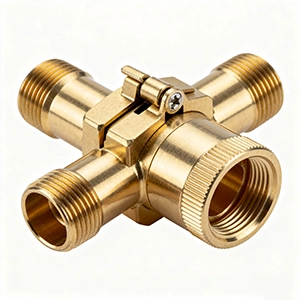
High-speed milling for valves, gear housings, and cosmetic faces. Balanced holders and light finish passes deliver bright surfaces ready for sealing or plating where required.

High-Precision Machining for Durable & Corrosion-Resistant Bronze Parts
Custom Prototypes and Production with Superior CNC Expertise
| Feature | Detail |
|---|---|
| Max Part Size (X/Y/Z) | 2300 × 1500 × 600 mm |
| Minimum Feature Size | ⌀1 mm |
| Wall Thickness | 0.25 mm |
| Tolerance | ±0.005 mm |
| Surface Finish (as milled) | Ra 0.4–3.2 µm |
| Standard Lead Time | 3 working-days for rapid prototyping |
| Pricing Level | To be confirmed after design review |
| Type of Machine | Gantry CNC / 3-4-5-Axis CNC / Mill-Turn Compound CNC / Swiss-Type CNC / Turning Machine...etc... |
| Bronze Grades | C932 (SAE 660 Bearing Bronze), C954 (Aluminum Bronze), C510 (Phosphor Bronze), C630 (Nickel-Aluminum Bronze) |
High-speed milling for valves, gear housings, and cosmetic faces. Balanced holders and light finish passes deliver bright surfaces ready for sealing or plating where required.
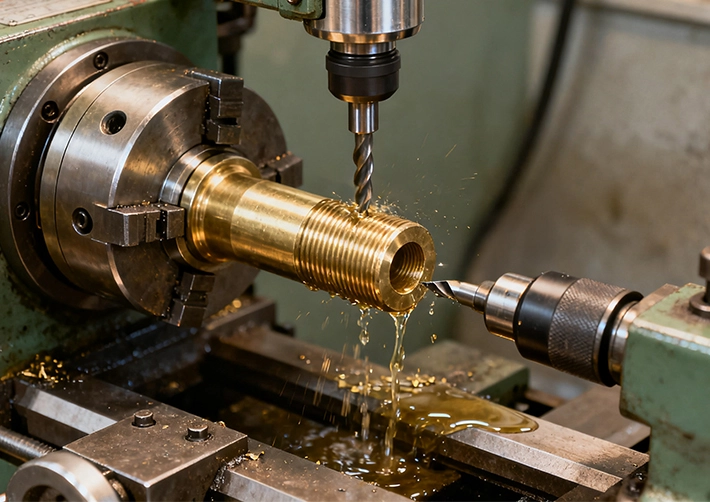
Fast, repeatable turning for bushings, sleeves, and bearing components. Mill-turn one-setup keeps concentricity tight and improves surface finish across features.
| Feature | Detail |
|---|---|
| Max Part Size (X/Y/Z) | 2300 × 1500 × 600 mm |
| Minimum Feature Size | ⌀1 mm |
| Wall Thickness | 0.25 mm |
| Tolerance | ±0.005 mm |
| Surface Finish (as milled) | Ra 0.4–3.2 µm |
| Standard Lead Time | 3 working-days for rapid prototyping |
| Pricing Level | To be confirmed after design review |
| Type of Machine | Gantry CNC / 3-4-5-Axis CNC / Mill-Turn Compound CNC / Swiss-Type CNC / Turning Machine...etc... |
| Bronze Grades | C932 (SAE 660 Bearing Bronze), C954 (Aluminum Bronze), C510 (Phosphor Bronze), C630 (Nickel-Aluminum Bronze) |
From free-cutting bearing bronzes to tough aluminum bronzes for high-load applications.
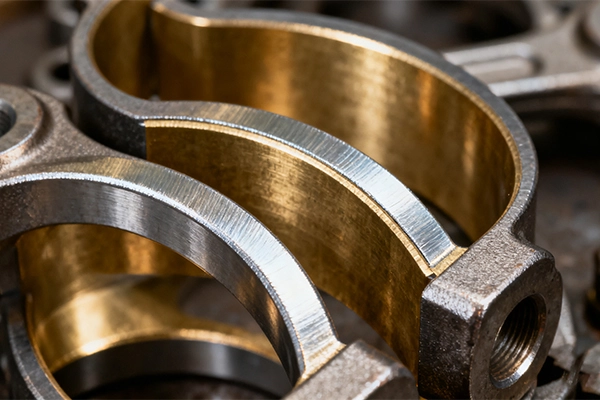
High SFM with sharp tools; chip-breakers help control stringers on lathes.
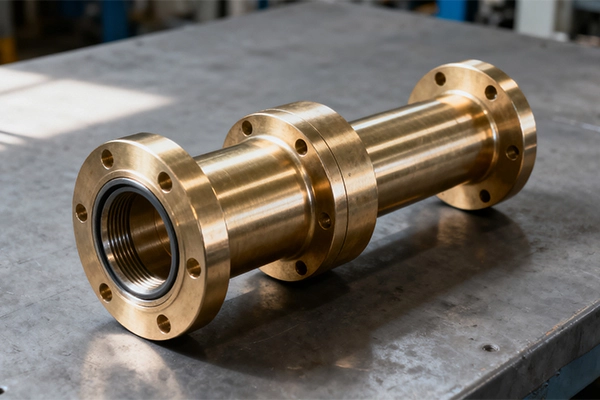
Moderate SFM with firm feed; use coated carbide and steady chip evacuation.
Use sharp edges and short stick-out; plan a light finish pass for flatness.
Lower SFM, strong chip load, coated carbide; consider stress relief on large parts.