
A 6 axis milling machine adds another degree of controlled movement beyond a typical 5-axis CNC machine. This gives the machine more freedom to position the cutting tool and workpiece when machining complex shapes, deep features, and difficult-to-reach surfaces.
However, more axes do not automatically mean better machining.
For many complex parts, a 5-axis CNC machine already provides enough tool access while keeping programming, setup, and machining costs under control. Six axis machining becomes useful when the part geometry truly needs the extra movement.
What Is a 6 Axis Milling Machine?
A 6 axis milling machine is a CNC machine that controls six axes of movement to machine complex parts from more directions.
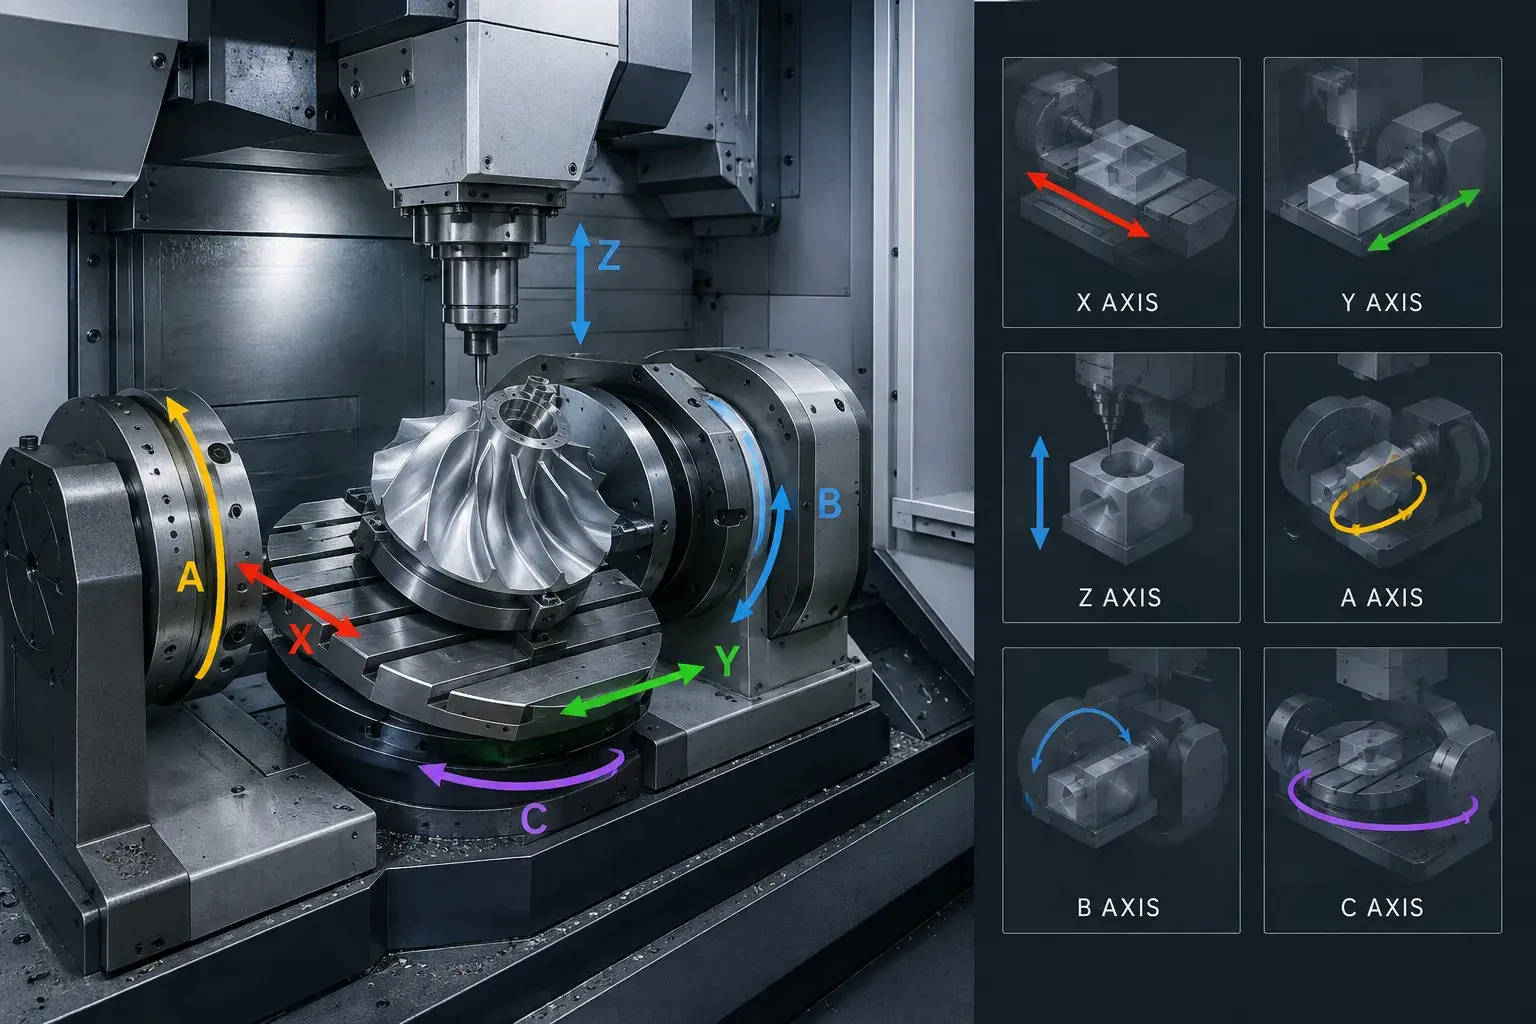
A 3-axis machine moves along X, Y, and Z, while a 5-axis machine adds two rotational axes. A 6-axis machine adds one more controlled movement, giving the tool or workpiece greater positioning freedom.
This can help machine deep undercuts, compound angles, twisted surfaces, and multi-sided features with fewer setups.
The exact six-axis configuration varies by machine design, so not every six axis CNC machine uses the same axis arrangement.
What Are the Six Axes in CNC Machining?
The six axes are usually described as three linear movements and three rotational movements.
The linear axes are:
- X-axis: left and right movement;
- Y-axis: forward and backward movement;
- Z-axis: up and down movement.
The rotational axes are:
- A-axis: rotation around the X-axis;
- B-axis: rotation around the Y-axis;
- C-axis: rotation around the Z-axis.
By combining linear and rotational motion, the machine can change the angle between the cutting tool and the workpiece while machining.
This gives the tool more ways to reach complex features without repeatedly removing and reclamping the part.
In practice, however, the actual axis arrangement depends on the machine design. Some machines rotate the table, some tilt the spindle, and others combine both methods. So “6-axis” describes the available controlled motion rather than one fixed machine structure.
How Does a 6 Axis Milling Machine Work?
A 6 axis milling machine combines linear and rotational movements so the cutting tool can reach the part from more directions.
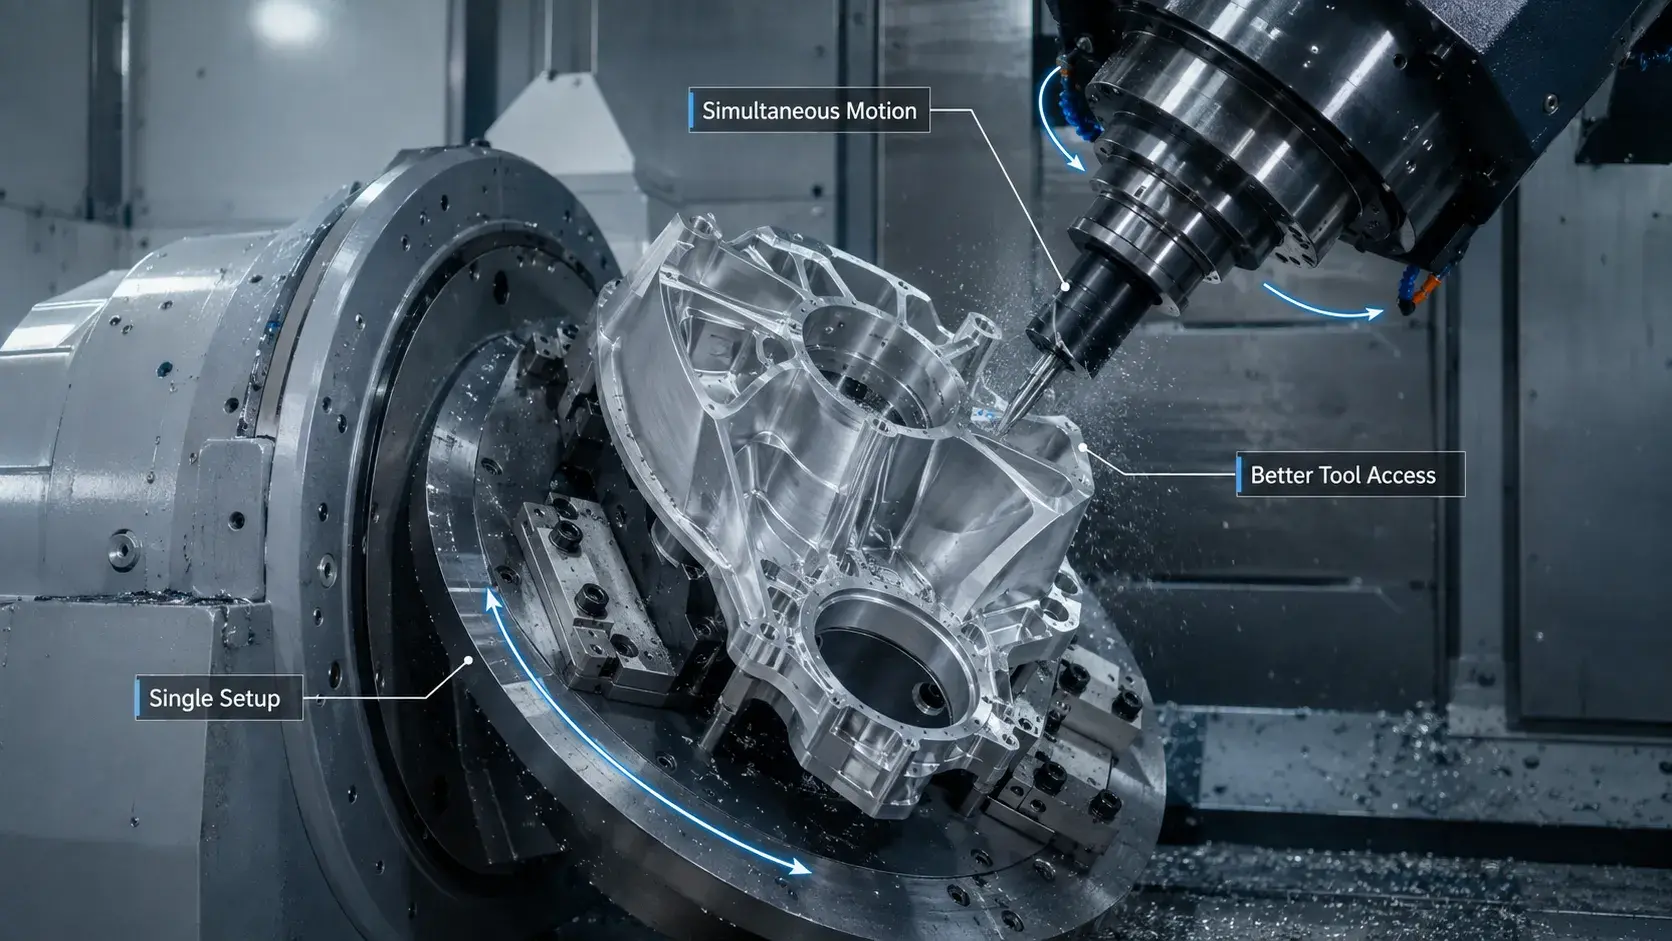
During machining, the CNC controller coordinates these movements based on the programmed toolpath. Depending on the machine design, the spindle, rotary table, or workpiece may move at the same time.
This extra freedom can reduce repositioning and help the cutter maintain a better angle when machining complex surfaces, deep features, and difficult areas.
For simple parts, this level of movement is usually unnecessary. The main advantage appears when the geometry becomes too complex for conventional 3-axis or even 5 axis machining.
True 6 Axis vs 5+1 Axis Machining
These two terms are often confused, but they are not the same.
In 5+1 axis machining, five axes are typically used for cutting while the sixth axis is mainly used to reposition or index the part.
In true 6 axis machining, all six controlled axes can participate in coordinated movement during the cutting process.
| Configuration | How It Works | Best For |
|---|---|---|
| 5-axis | Five controlled axes | Most complex CNC parts |
| 5+1 axis | Five cutting axes plus one positioning axis | Multi-sided parts and flexible setups |
| True 6-axis | Six coordinated axes | Very complex geometry and difficult tool access |
For many parts, 5-axis or 5+1 machining is already enough. True 6-axis machining is usually reserved for applications where the additional motion provides a clear machining advantage.
5 Axis vs 6 Axis CNC Machining
The biggest difference between 5 axis and 6 axis CNC machining is the amount of movement available during cutting.
A 5-axis machine already gives the tool enough freedom to reach most complex surfaces from different angles. A 6 axis machine adds another controlled movement, which can help with parts that have more difficult geometry or limited tool access.
| Comparison | 5-Axis CNC | 6-Axis CNC |
|---|---|---|
| Controlled movement | 5 axes | 6 axes |
| Tool access | Excellent | Greater flexibility |
| Part complexity | Handles most complex parts | Better for very difficult geometry |
| Setup requirements | Usually very low | Can reduce setups further |
| Programming | Complex | More complex |
| Collision risk | High if poorly programmed | Even higher |
| Machine cost | High | Usually higher |
| Typical use | Aerospace, medical, molds, impellers | Specialized complex components |
For most precision parts, 5-axis machining is the more practical choice. It offers strong tool access, fewer setups, and high machining flexibility without the extra cost and programming complexity of a 6-axis system.
Six-axis machining makes more sense when the additional axis solves a real problem, such as reaching a difficult feature, avoiding tool interference, or machining highly complex surfaces more efficiently.
Advantages of 6 Axis Milling
The main benefit of 6-axis milling is greater machining freedom.
With an additional controlled axis, the machine may be able to reach difficult areas without removing and reclamping the workpiece. This can be useful for parts with complex curves, undercuts, deep features, and multiple machining angles.
Other possible advantages include:
- fewer setups for complex parts;
- better access to hard-to-reach features;
- more flexible tool orientation;
- improved machining of compound surfaces;
- reduced repositioning between operations;
- shorter cycle times for some complex parts.
However, 6-axis machining is not automatically more accurate than 5-axis machining. Final accuracy still depends on machine rigidity, calibration, tooling, fixturing, thermal stability, and the machining strategy.
Limitations of 6 Axis Machining
Six-axis machining offers more freedom, but it also adds cost and complexity.
The main limitations include:
- higher machine cost;
- more complex CAM programming;
- greater collision risk;
- higher maintenance requirements;
- more demanding setup and calibration;
- need for experienced programmers and operators.
For many parts, the extra axis does not provide enough benefit to justify these added costs. If a 5-axis machine can reach all required features in one or two setups, it is often the more efficient option.
What Parts Need 6 Axis Machining?
Six-axis machining is mainly useful for parts with geometry that is difficult to reach using conventional multi-axis machines.
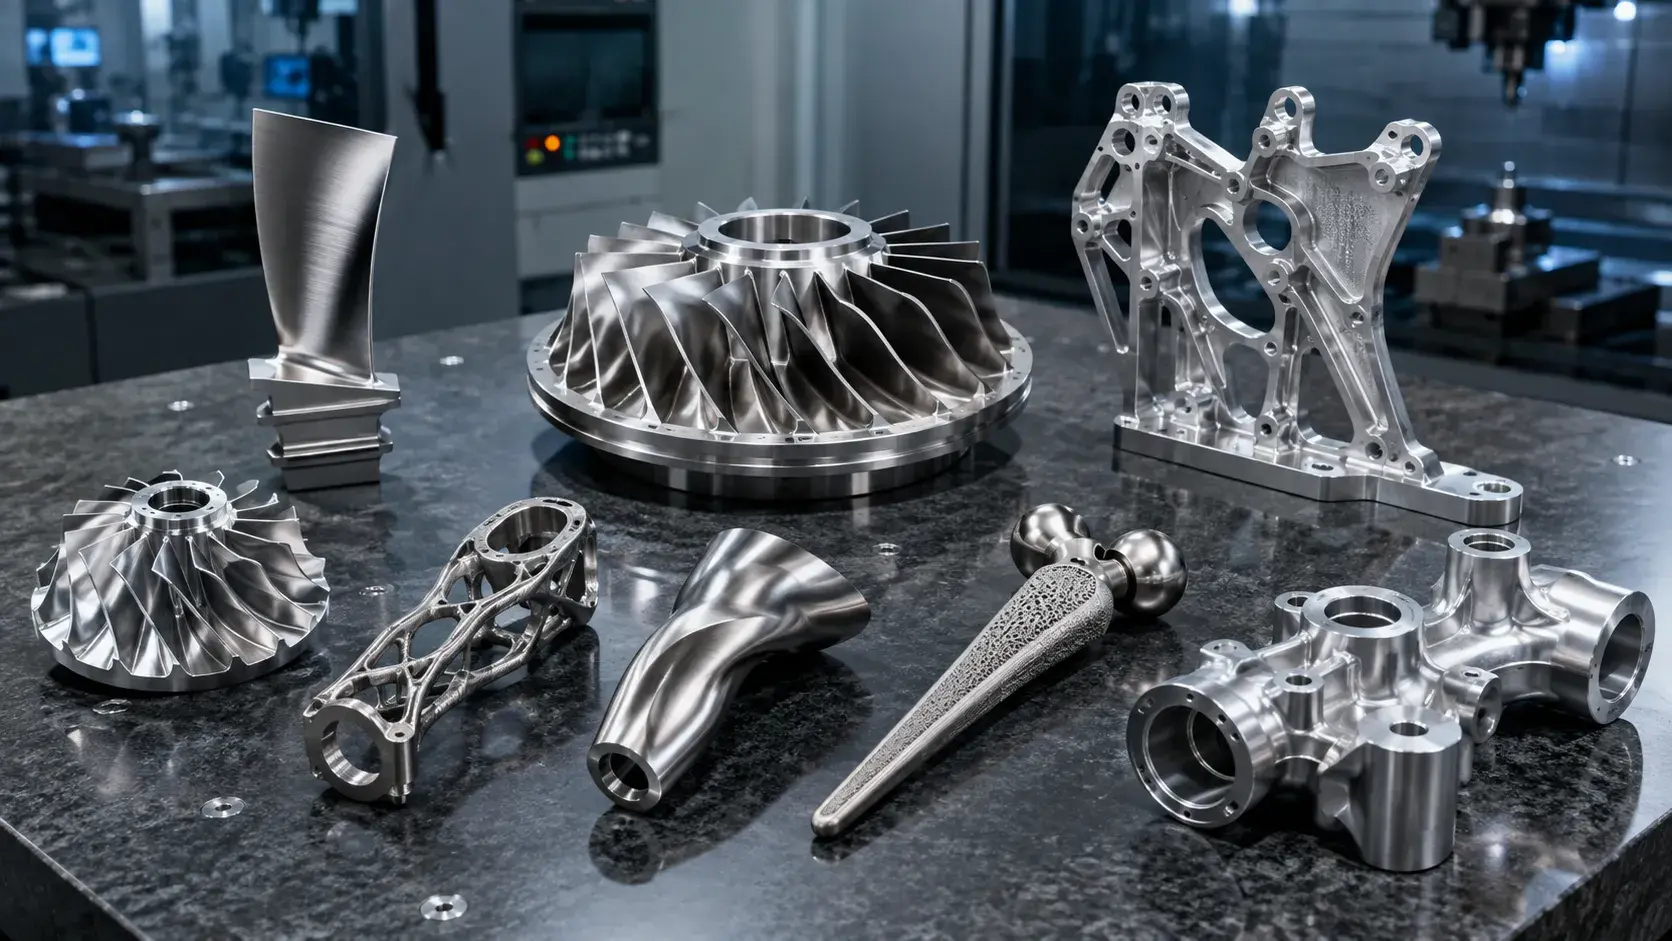
Typical examples include:
- turbine blades and blisks;
- complex impellers;
- aerospace structural components;
- parts with deep undercuts;
- components with twisted or compound surfaces;
- complex medical and orthopedic parts;
- turbine and compressor components.
The important point is that not every complex part needs six axes.
Many housings, brackets, molds, impellers, and multi-sided parts can already be machined efficiently with 5-axis CNC. Six-axis machining is most useful when the additional movement directly improves tool access or reduces otherwise difficult setups.

6 Axis Milling Machine vs 6 Axis Robot
A 6-axis milling machine and a 6-axis robot both move in six directions, but they are built for different types of work.
A 6-axis CNC machine is designed for rigid, high-precision cutting of metal parts. It is better suited to tight tolerances, stable surface finishes, and demanding machining operations.
A 6-axis robot offers a much larger working range and greater flexibility, but it usually has lower rigidity and machining accuracy.
| Comparison | 6-Axis CNC Machine | 6-Axis Robot |
|---|---|---|
| Rigidity | High | Lower |
| Machining accuracy | High | Usually lower |
| Working range | Smaller | Much larger |
| Best for | Precision metal machining | Trimming, drilling, composites, large parts |
| Typical materials | Aluminum, steel, titanium | Composites, plastics, foam, softer materials |
For precision metal parts, a CNC machining center is usually the better choice. Robotic machining is more useful when reach, flexibility, or part size is more important than very tight machining accuracy.
How Much Does a 6 Axis Milling Machine Cost?
A 6-axis milling machine is usually more expensive than a standard 3-axis or 5-axis machine because of its additional motion system, control requirements, and machine complexity.
Industrial multi-axis machining centers can range from several hundred thousand dollars to more than $1 million, depending on the configuration.
The final price is affected by factors such as:
- machine size and travel;
- spindle speed and power;
- rotary axis design;
- CNC control system;
- tool capacity;
- probing and measurement systems;
- pallet or automation options.
Used machines may cost much less, while large high-end systems with automation can exceed this range.
For a machining buyer, however, the more important question is usually not the machine purchase price but whether the extra axis can reduce setups, cycle time, or production risk enough to justify the higher machining cost.
Do You Really Need 6 Axis Machining?
Not every complex part needs a 6-axis machine.
If all critical features can be reached with 5-axis machining, the tolerances can be held reliably, and the number of setups is already low, then 5-axis is usually the more practical option.
Six-axis machining becomes more useful when:
- important features are difficult to reach;
- tool interference limits the cutting angle;
- the part has deep undercuts or complex compound surfaces;
- multiple setups may affect feature-to-feature accuracy;
- the extra axis can reduce machining time or simplify the process.
For most precision CNC parts, 5-axis machining provides a good balance between flexibility, accuracy, and cost. Six-axis machining is better treated as a specialized solution for geometry that genuinely needs the extra movement.
Conclusion
A 6 axis milling machine provides more motion and tool-access flexibility than a 5-axis machine, but that does not mean it is always the better choice.
For most complex parts, 5 axis CNC machining is already capable of reducing setups, reaching multiple surfaces, and maintaining high accuracy. Six-axis machining is most valuable when the additional axis solves a specific problem that 5-axis machining cannot handle efficiently.
When choosing between 5-axis and 6-axis machining, the part geometry, tolerance requirements, setup strategy, and production cost matter more than the number of axes alone.



