

The main types of CNC machines include CNC mills, lathes, Swiss machines, mill-turn centers, gantry machines, routers, EDM machines, drilling machines, and CNC grinders.
The right choice depends on your part geometry, size, tolerance, material, and production volume. A round shaft may suit a lathe, while a complex multi-surface part may require 5-axis machining.
Quick Comparison of CNC Machine Types
| CNC Machine Type | Best For | Typical Parts | Main Advantage |
|---|---|---|---|
| CNC Milling Machine | Prismatic parts | Housings, brackets, plates | Flexible machining |
| CNC Lathe | Round parts | Shafts, bushings, sleeves | Efficient turning |
| Swiss CNC Machine | Small, slender parts | Pins, connectors, small shafts | High precision and support |
| Mill-Turn Machine | Mixed turned and milled geometry | Complex shafts, fittings | Fewer setups |
| Gantry CNC Machine | Large parts | Frames, large plates, bases | Large work envelope |
| CNC Router | Soft materials and panels | Plastics, composites, wood | High speed |
| CNC Drilling/Tapping Machine | Hole-intensive parts | Plates, covers, flanges | Fast hole production |
| CNC EDM Machine | Hard materials and fine features | Dies, narrow slots | No cutting force |
| CNC Grinding Machine | Final finishing | Shafts, hardened parts | Tight tolerance and fine finish |
1. CNC Milling Machines
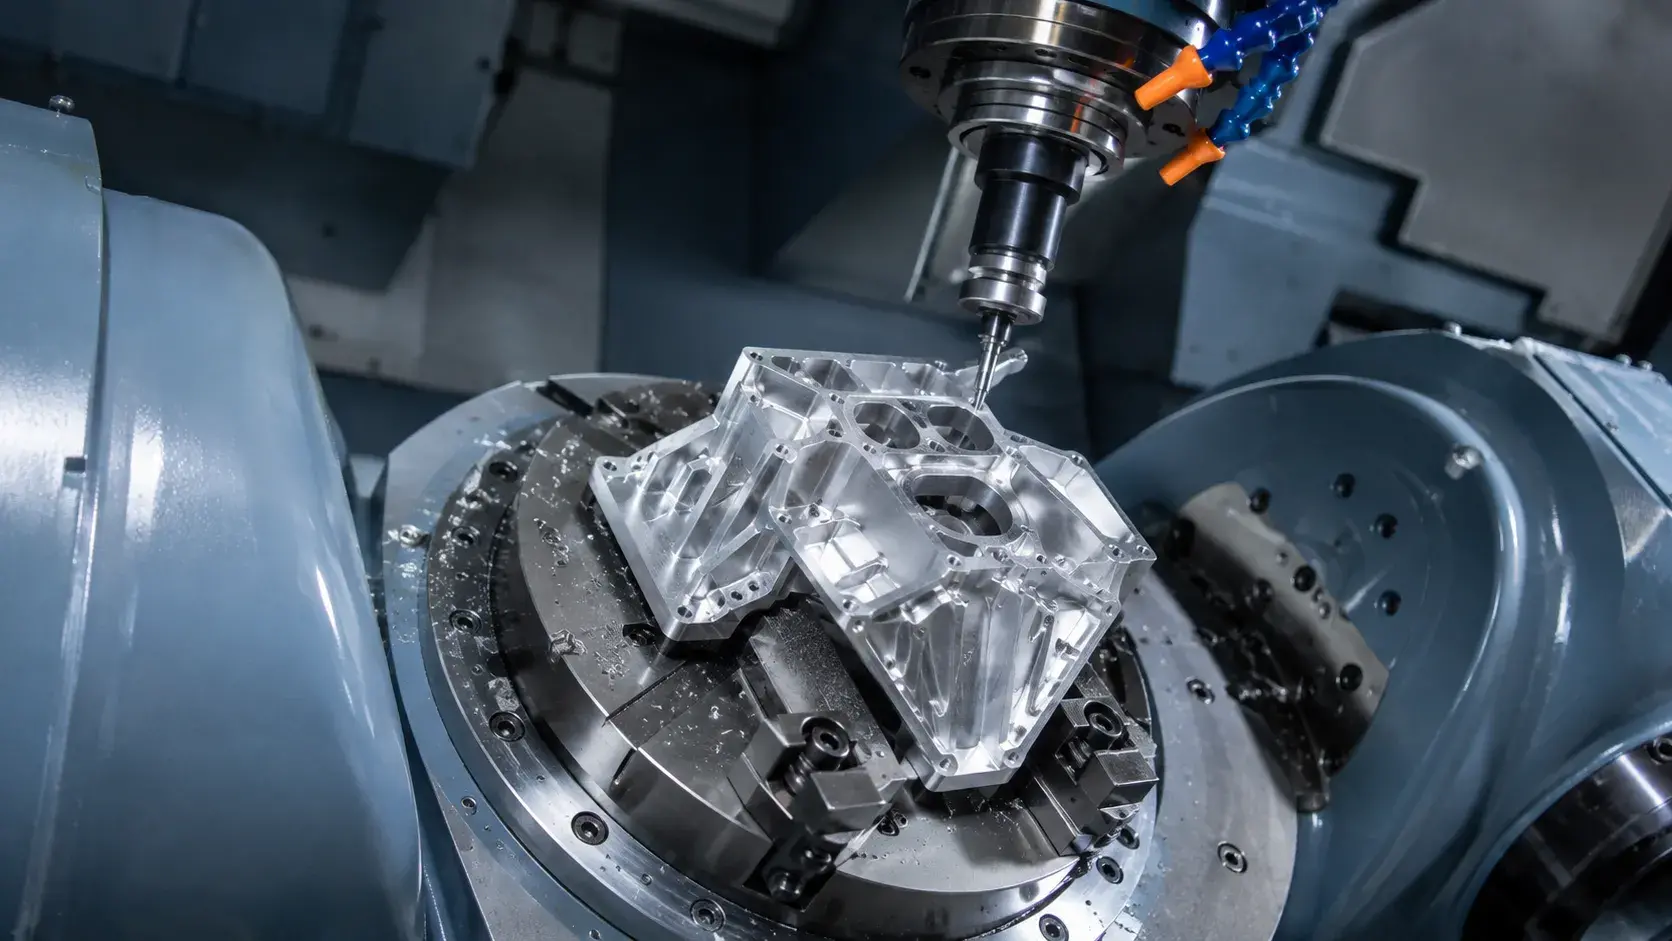
CNC milling machines use rotating cutting tools to remove material from a stationary workpiece.
They are commonly used for parts that contain:
- Pockets
- Holes
- Slots
- Flat surfaces
- Threads
- Contours
- Multiple machined faces
Typical parts include aluminum housings, brackets, plates, fixtures, and machine components.
CNC milling machines may use 3, 4, or 5 axes depending on part complexity. A simple rectangular part may only need 3-axis machining, while a complex aerospace bracket may require 5-axis access.
The important point is that 3-axis, 4-axis, and 5-axis machines are not completely separate machining processes. They are different axis configurations within CNC milling.
2. CNC Lathes and Turning Centers
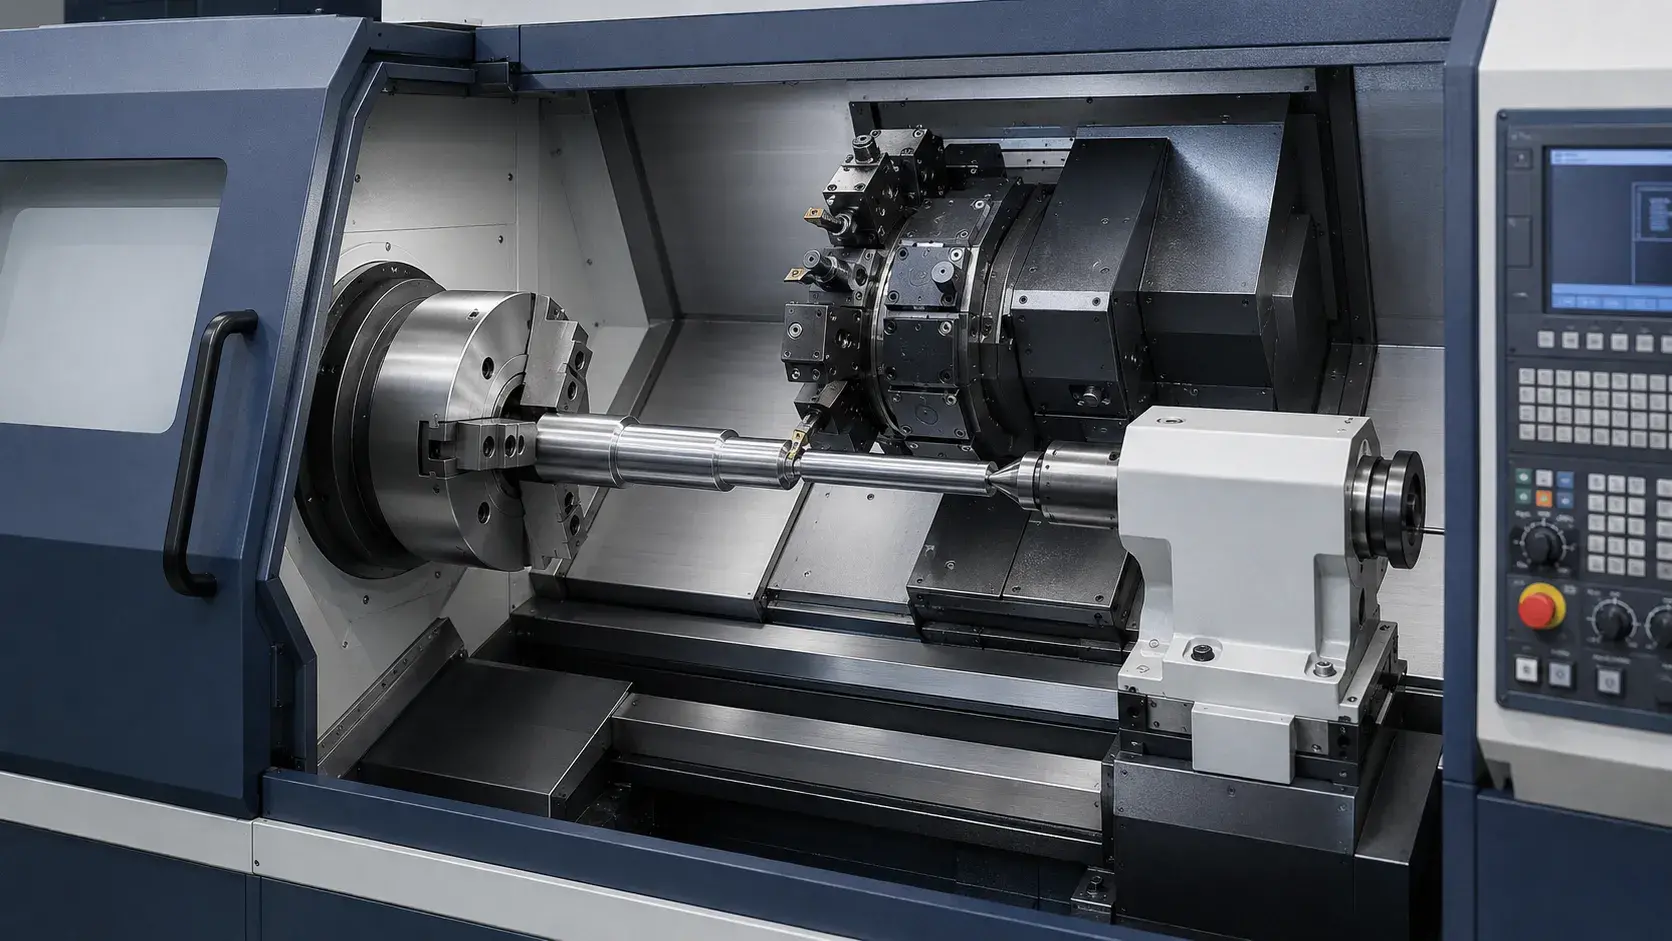
A CNC lathe rotates the workpiece while a cutting tool removes material.
This makes it ideal for parts that are mainly round or cylindrical.
Common examples include:
- Shafts
- Bushings
- Sleeves
- Pins
- Spacers
- Nozzles
- Threaded components
Turning is generally faster and more efficient than milling for rotational parts because the machine is designed around the geometry of the part.
Modern CNC turning centers can also include live tooling, allowing some drilling, milling, or tapping operations without moving the part to another machine.
If most of your component is symmetrical around a centerline, CNC turning is usually one of the first processes to consider.
3. Swiss CNC Machines
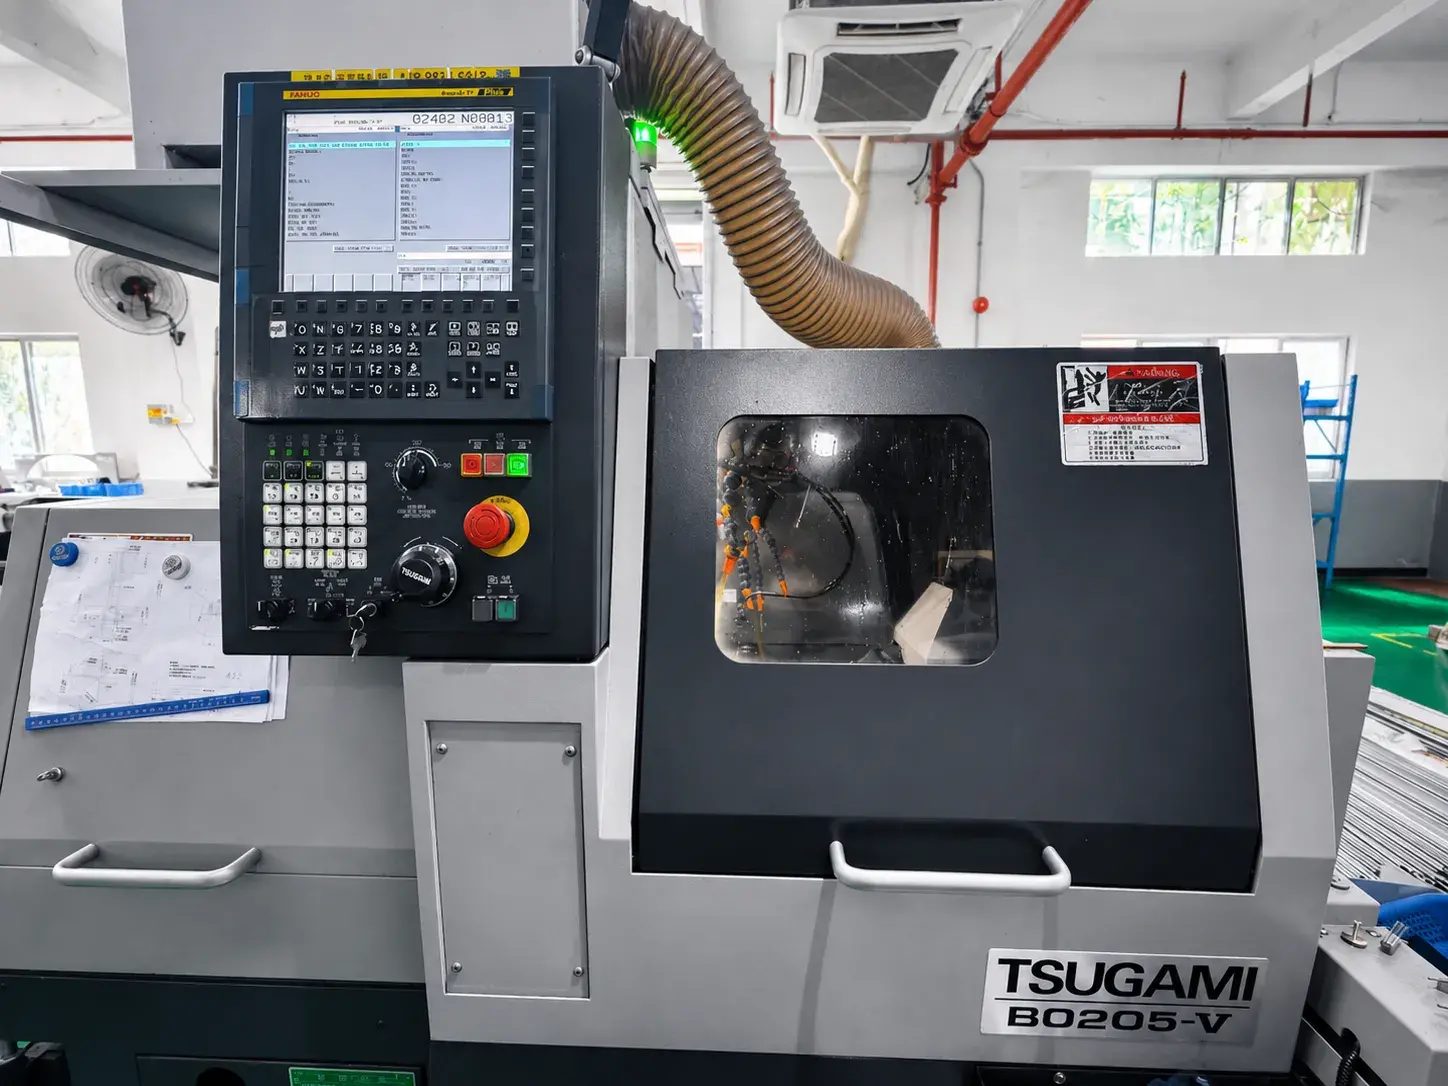
Swiss CNC machines are a specialized type of turning machine designed for small, long, and high-precision parts.
The key difference is support.
On a conventional lathe, a long thin part may bend or vibrate during cutting. A Swiss machine supports the workpiece close to the cutting area using a guide bushing, reducing deflection.
Swiss machining is especially suitable for:
- Small pins
- Long slender shafts
- Connectors
- Medical components
- Small threaded parts
- Precision fittings
It is particularly useful when diameter is small relative to part length.
For example, a part around Ø5 mm × 160 mm is much more difficult to machine accurately on a conventional lathe because of deflection. Swiss machining is often a better choice for this type of geometry.
Swiss machines are also well suited to higher-volume production because they are commonly bar-fed and can perform several operations in one cycle.
4. Mill-Turn CNC Machines
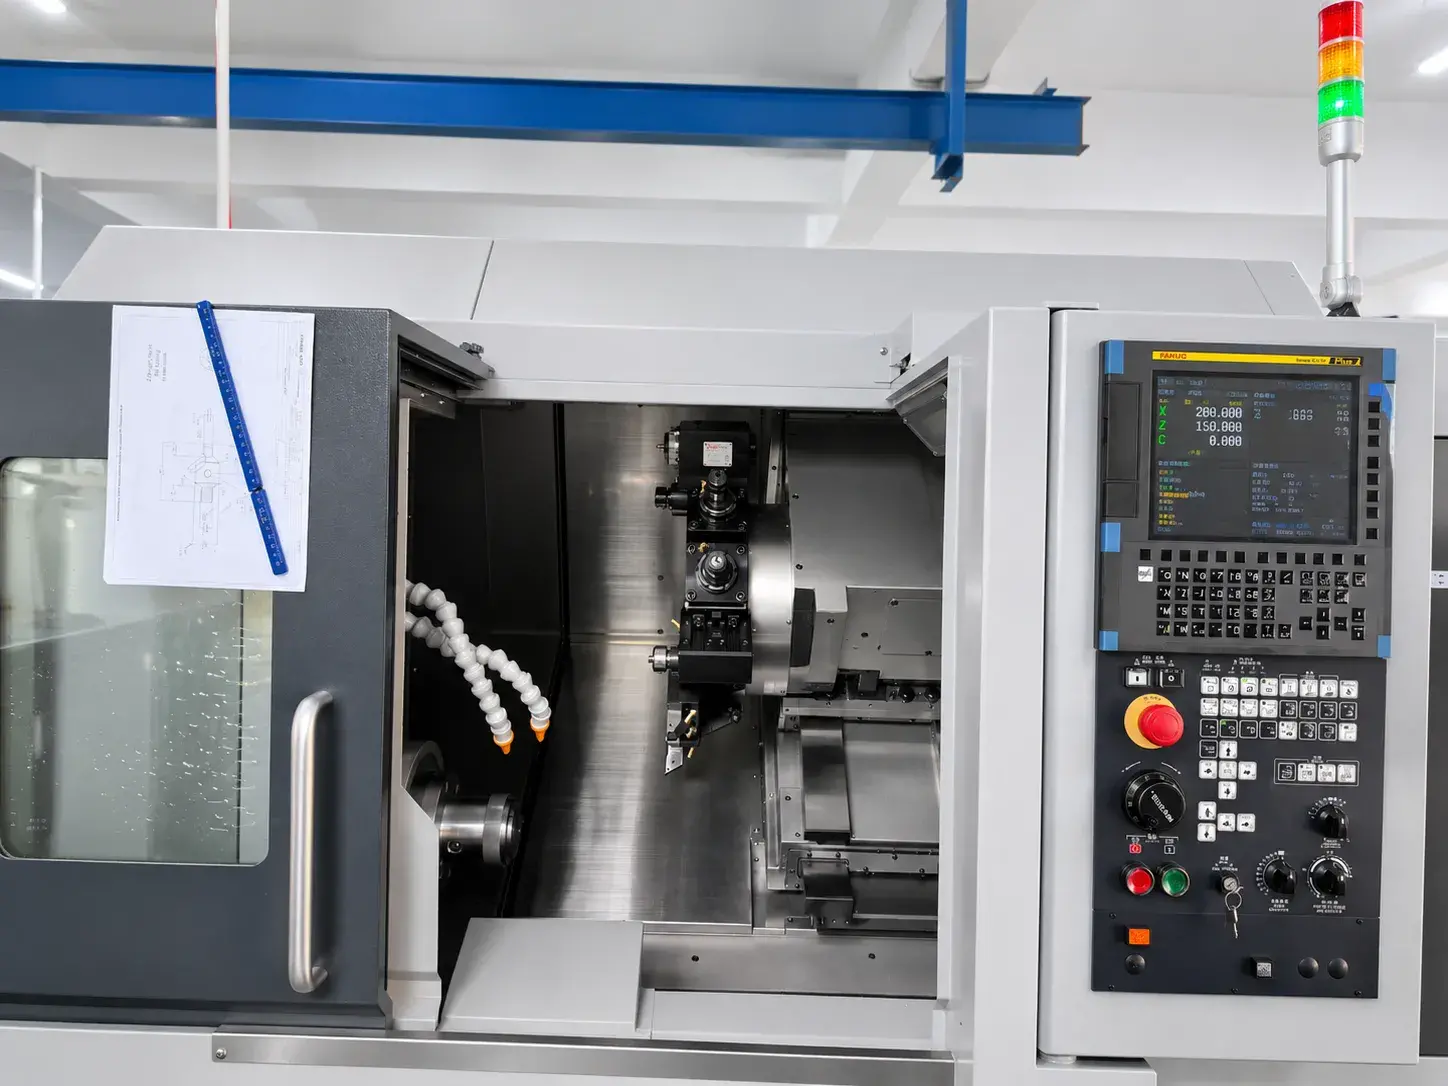
Mill-turn machines combine turning and milling in one machine.
They are useful for parts that are mainly rotational but also require features such as:
- Flats
- Cross holes
- Slots
- Off-center holes
- Milled faces
- Complex threads
A conventional production route might require turning the part first, then moving it to a milling machine.
A mill-turn machine can often complete both operations in one setup.
That matters because every additional setup introduces more handling, fixturing, alignment, and possible dimensional variation.
Typical mill-turn parts include complex shafts, hydraulic fittings, aerospace components, and precision mechanical parts with both round and non-round features.
5. Gantry CNC Machines
Gantry CNC machines are designed for large workpieces.
Instead of fitting a part into a standard machining center, the machine structure spans across a large work area.
Typical applications include:
- Large aluminum plates
- Machine bases
- Structural frames
- Fixtures
- Large housings
- Industrial equipment components
Gantry machines are often chosen because of part size rather than part complexity.
A relatively simple part may still require a gantry machine if it is too large for a standard vertical machining center.
For large components, machine travel and table capacity are often the first things to check before tolerance or toolpath complexity.
6. CNC Routers
CNC routers operate in a similar way to CNC milling machines, but they are usually optimized for high-speed machining of softer materials and larger flat workpieces.
Common materials include:
- Wood
- Plastics
- Foam
- Composites
- Soft aluminum sheets
CNC routers are widely used for panels, signage, plastic sheets, composite parts, and woodworking.
Compared with a heavy CNC machining center, a router usually has lower rigidity and is less suited to demanding precision machining of steel, stainless steel, or other hard metals.
For precision metal components with tight tolerances, a CNC milling machine is usually the better choice.
7. CNC Drilling and Tapping Machines
CNC drilling and tapping machines are optimized for fast hole-making operations.
They are useful for parts that require:
- Repeated hole patterns
- Tapped holes
- Counterbores
- Spot drilling
- Production drilling
Typical examples include covers, plates, flanges, and simple production components with many holes.
These machines are often selected for speed and efficiency rather than complex 3D machining.
If a component is mostly flat and contains many repeated drilled and tapped features, a drilling and tapping center can be more economical than using a larger general-purpose machine.
8. CNC EDM Machines
EDM stands for Electrical Discharge Machining.
Instead of cutting material with a conventional tool, EDM removes conductive material using controlled electrical sparks.
The two common types are:
- Wire EDM
- Sinker EDM
EDM is useful when conventional cutting becomes difficult.
Typical applications include:
- Hardened steel
- Narrow slots
- Fine internal details
- Die and mold components
- Small radii
- Delicate features
One major advantage is that EDM does not apply normal cutting force to the workpiece.
This makes it useful for thin or delicate features that could bend during conventional machining.
However, EDM only works with electrically conductive materials.
9. CNC Grinding Machines
CNC grinding machines are generally used for final finishing rather than removing large amounts of material.
Grinding is useful when a component needs:
- Very tight dimensional control
- Fine surface finish
- High roundness
- Precision cylindrical surfaces
- Machining after heat treatment
Typical parts include precision shafts, bearing surfaces, hardened components, and tooling.
A part may first be turned or milled close to final size, then ground to achieve the required finish and dimensional accuracy.
For this reason, grinding often works as a secondary or finishing process rather than the main manufacturing method.
How to Choose the Right CNC Machine
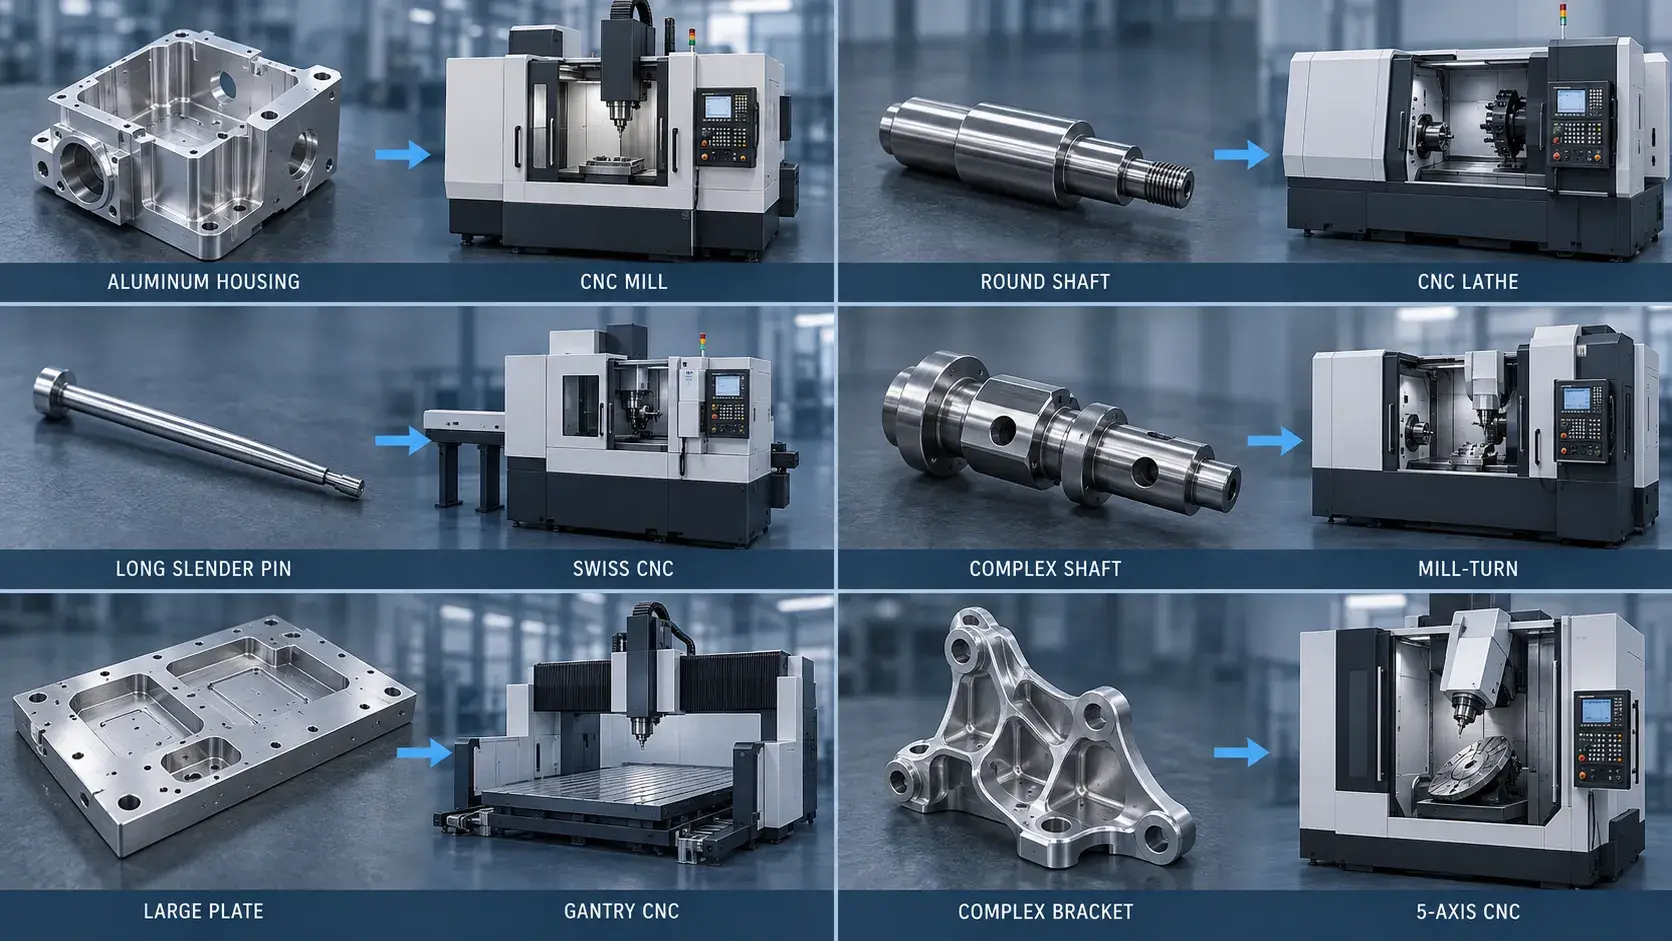
The best machine should be selected around the part rather than the equipment itself.
1. Start With Part Geometry
Part shape is often the fastest way to narrow down the process.
- Mostly round parts: CNC lathe
- Small, long, slender parts: Swiss CNC
- Box-shaped or prismatic parts: CNC milling
- Round parts with milled features: Mill-turn
- Large parts: Gantry CNC
- Complex multi-surface parts: 5-axis CNC
2. Consider Machined Sides and Setup Count
A simple part with easily accessible features may only need 3-axis machining.
If the part requires machining around several sides or angled surfaces, 4-axis or 5-axis machining may reduce repositioning and setup count.
Fewer setups can improve feature-to-feature consistency and reduce handling.
3. Check Part Size
Part size can eliminate some machine options immediately.
Large plates, housings, or structural components may require a gantry machine, while small precision parts may be more efficiently produced on Swiss or compact turning equipment.
Always check machine travel, table size, workholding space, and part weight.
4. Consider Tolerance and Production Volume
Tight tolerances do not automatically require the most advanced machine. Machine condition, workholding, tooling, inspection, and setup count all affect accuracy.
Production volume also matters. Flexible machines often suit prototypes and small batches, while Swiss machining and automation can be more economical for repetitive production.
CNC Machine Selection by Part Type
The following table gives a practical starting point.
| Part Type | Recommended Starting Choice |
|---|---|
| Aluminum housing | 3-axis or 5-axis CNC mill |
| Simple bracket | 3-axis CNC mill |
| Multi-side bracket | 4-axis CNC mill |
| Complex aerospace bracket | 5-axis CNC mill |
| Shaft | CNC lathe |
| Bushing | CNC lathe |
| Long precision pin | Swiss CNC |
| Small connector | Swiss CNC |
| Shaft with flats and cross holes | Mill-turn |
| Large aluminum plate | Gantry CNC |
| Large machine base | Gantry CNC |
| Hardened narrow slot | Wire EDM |
| Complex mold cavity | Sinker EDM |
| Precision finished shaft | CNC grinding |
This table is only a starting point. Material, tolerance, surface finish, quantity, and feature complexity can change the final process choice.
3-Axis vs 4-Axis vs 5-Axis: Are They Different CNC Machine Types?
3-axis, 4-axis, and 5-axis are better understood as different configurations of CNC milling rather than completely separate machining families.
Additional axes provide better access to multiple faces and complex angles, which can reduce setups and repositioning.
Do You Need the Most Advanced CNC Machine?
No.
The most advanced machine is not automatically the best machine for every part.
A simple aluminum plate with pockets and holes may be faster and cheaper to machine on a 3-axis machining center.
Using a 5-axis machine may add programming cost without providing much benefit.
On the other hand, forcing a complex part onto a simpler machine can create other costs:
- More fixtures
- More setups
- More manual handling
- Longer lead time
- Higher inspection effort
- Greater risk of cumulative positioning error
The right machine is the one that produces the required geometry and tolerance with the fewest unnecessary steps.
Final Thoughts
There is no single CNC machine that is best for every component.
CNC mills are strong all-around choices for prismatic parts. Lathes are best for round components. Swiss machines are excellent for long, small-diameter parts. Mill-turn centers reduce setups for complex rotational parts, while gantry machines handle large components.
EDM and grinding solve more specialized problems where conventional milling or turning may not be enough.
The best way to choose is to start with your part geometry, then consider size, tolerance, setup count, material, and production volume.
If you already have a CAD model or drawing, the machine should be selected based on the part—not the other way around.



