

Metal punching and stamping are both common sheet metal processes, but they are not the same.
Punching mainly removes material to create holes, slots, cutouts, and similar features. Stamping is a broader process that can include punching, blanking, bending, embossing, flanging, and deep drawing.
In simple terms, punching focuses mainly on cutting features into sheet metal, while stamping can both cut and reshape the material.
Punching vs Stamping at a Glance
| Factor | Metal Punching | Metal Stamping |
|---|---|---|
| Main purpose | Create holes, slots, and cutouts | Cut and form sheet metal |
| Typical geometry | Mostly flat sheet parts | Flat and formed parts |
| Tooling | Punch and die, often standard or turret tools | Dedicated dies commonly used |
| Setup cost | Low to medium | Medium to high |
| Design flexibility | Relatively high | Lower after tooling is completed |
| Best volume | Prototype to medium/high volume | Medium to very high volume |
| Typical features | Holes, slots, louvers, knockouts | Bends, ribs, flanges, cups, shells |
| Design changes | Easier | Often require die modification |
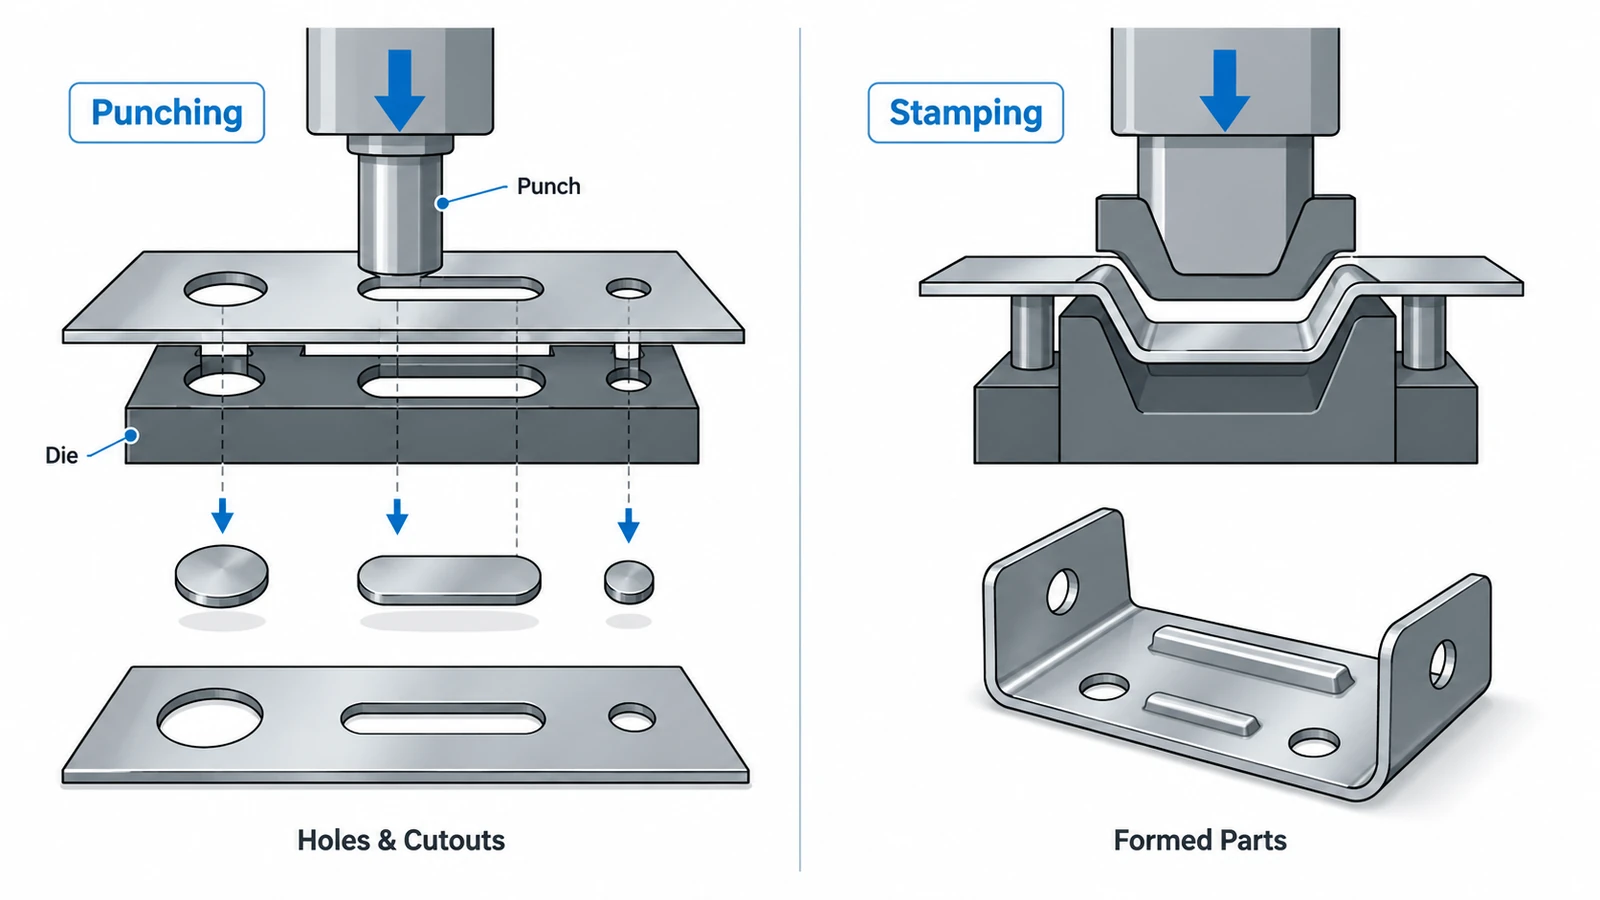
The key relationship is simple: punching can be one operation within a stamping process.
What Is Metal Punching?
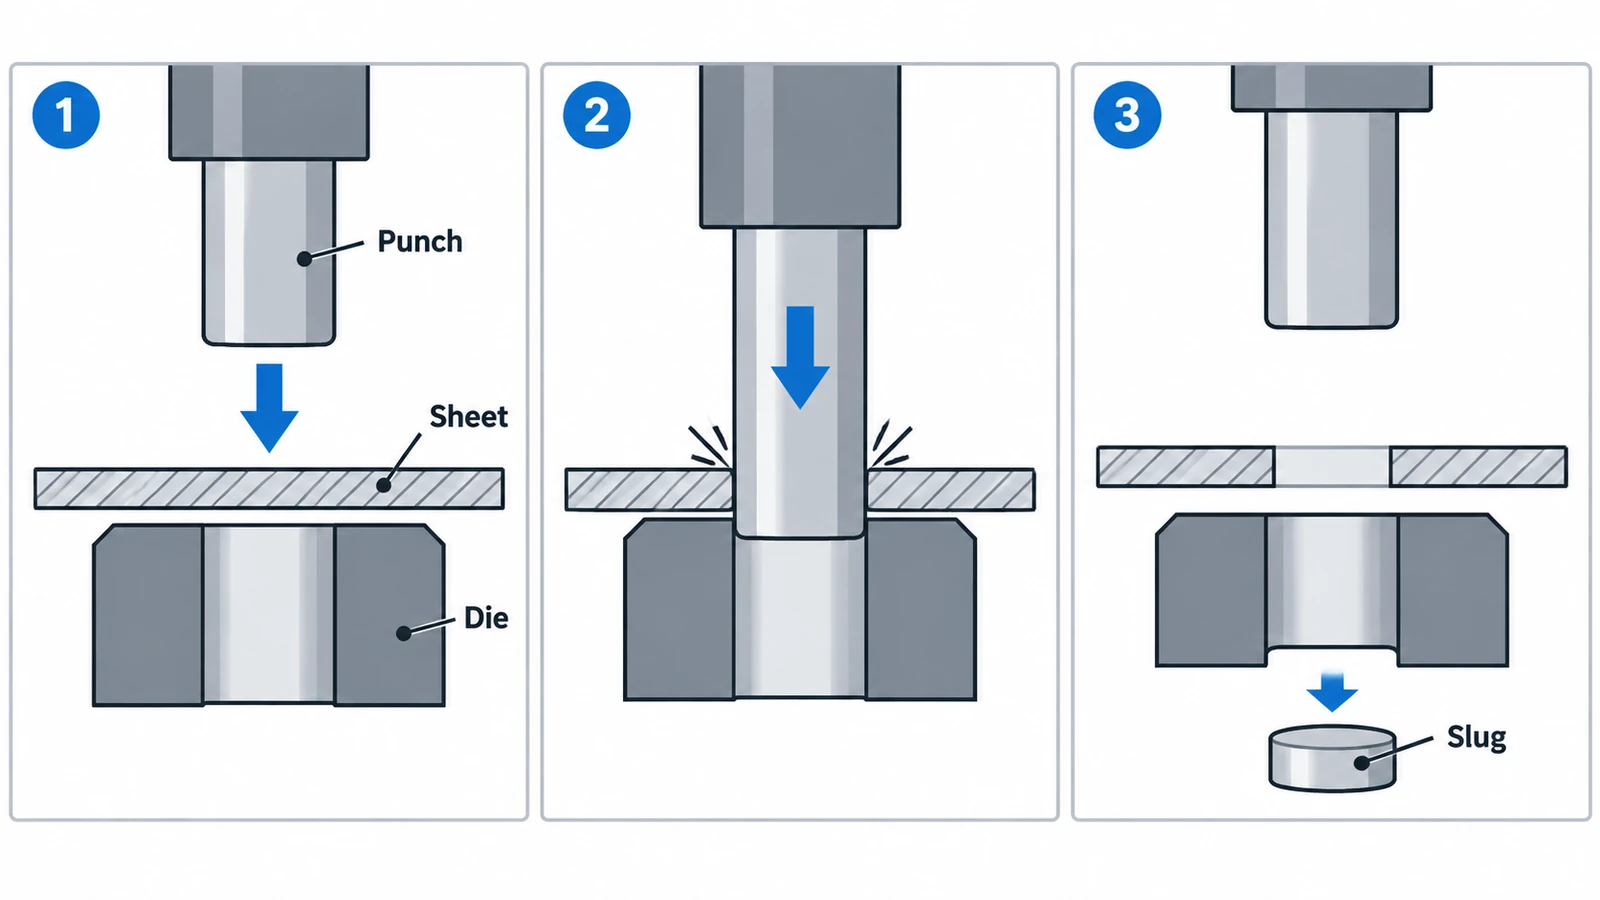
Metal punching is a sheet metal cutting process in which a punch forces the sheet into a matching die opening. The shearing action removes material and creates a hole or cutout.
Modern CNC turret punching can produce more than simple round holes. Typical features include:
- Round and square holes
- Slots
- Perforation patterns
- Cable openings
- Knockouts
- Louvers
- Extruded holes
- Embossed features
Punching is particularly effective for mostly flat parts containing many repeated features.
Its performance depends on tool geometry, sheet thickness, material strength, and punch-to-die clearance.
What Is Metal Stamping?
Metal stamping uses presses and dies to cut or form sheet metal into a required shape.
Common stamping operations include:
- Punching
- Blanking
- Bending
- Flanging
- Embossing
- Coining
- Deep drawing
Stamping can therefore create much more three-dimensional geometry than punching alone.
For high-volume production, progressive dies can combine several operations in sequence, such as punching holes, bending flanges, forming ribs, and cutting the finished part from the strip.
6 Key Differences Between Punching and Stamping
1. Purpose
Punching mainly removes material.
Typical results include holes, slots, cutouts, and perforations.
Stamping can both remove and reshape material, allowing features such as bends, ribs, flanges, shells, and drawn sections.
2. Part Geometry
Punching is best suited to flat or mostly flat sheet-metal parts.
Stamping is better when the component requires formed three-dimensional geometry.
For example, an electrical panel with many holes may be punched, while an automotive bracket with bends and ribs is more likely to be stamped.
3. Tooling
Punching usually uses individual punch-and-die sets or turret tooling.
This gives manufacturers relatively good flexibility when hole patterns or features change.
Stamping often uses dedicated dies designed specifically for one part.
These tools cost more to develop, but they can combine several operations and produce parts very quickly once production begins.
4. Production Volume
Punching can work well from prototypes through medium and relatively high production volumes.
Stamping becomes more attractive as production volume increases because the tooling cost is spread across more parts.
There is no universal break-even quantity. It depends on:
- Tooling complexity
- Material
- Part geometry
- Number of operations
- Cycle time
- Production quantity
5. Cost Structure
Punching generally has a lower initial tooling cost.
However, punched parts may still require secondary bending, tapping, deburring, welding, or machining.
Stamping usually requires higher upfront tooling investment, but it can achieve very low unit costs in large production runs.
A simple way to think about it is:
Punching = lower tooling cost and higher flexibility.
Stamping = higher tooling cost and better high-volume efficiency.
6. Design Changes
Punching is generally easier to adapt when a design changes.
Hole positions or cutout patterns can often be updated through programming and tool selection.
Stamping is less flexible once the die has been completed. Changes to bend locations, flanges, holes, or overall geometry may require die modification or new tooling.
For this reason, flexible processes are often preferred during product development before a design is frozen for mass production.
Typical Punching and Stamping Applications
| Punching Applications | Stamping Applications |
|---|---|
| Electrical enclosures | Automotive brackets |
| Ventilation panels | Clips |
| Server rack panels | Connector shells |
| Mounting plates | Structural sheet parts |
| Perforated guards | Covers and shields |
| Cable-entry panels | Electrical terminals |
| Flat brackets | Deep-drawn housings |
| Equipment panels | Appliance components |
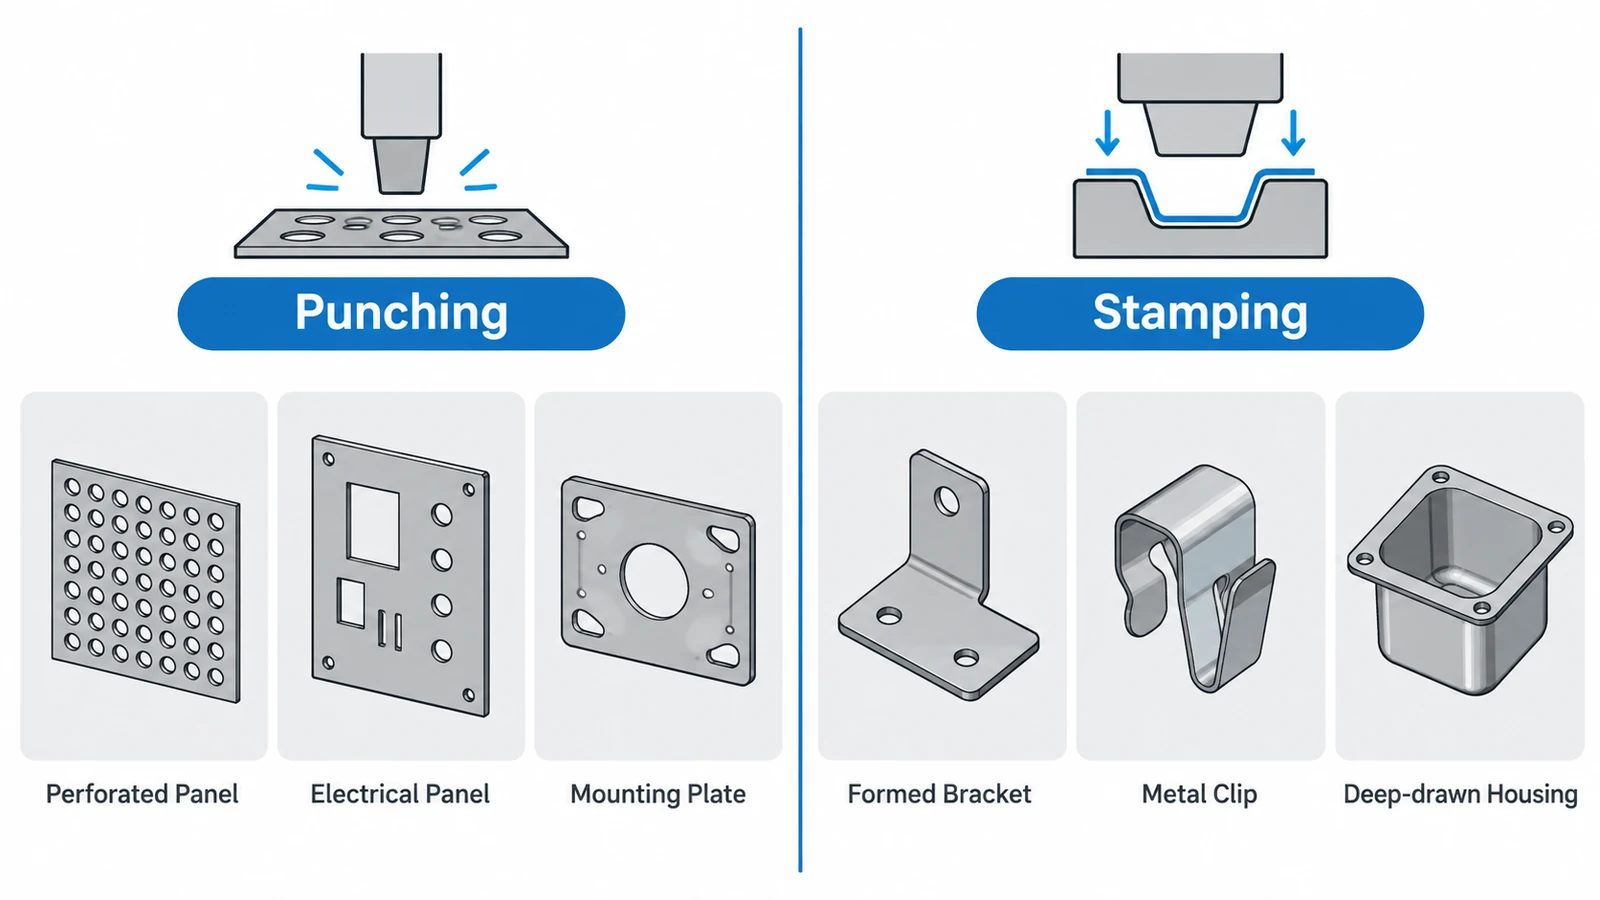
Punching is especially efficient for parts containing many repeated holes or openings.
Stamping is more suitable when the part needs several formed features and will be manufactured repeatedly in large quantities.
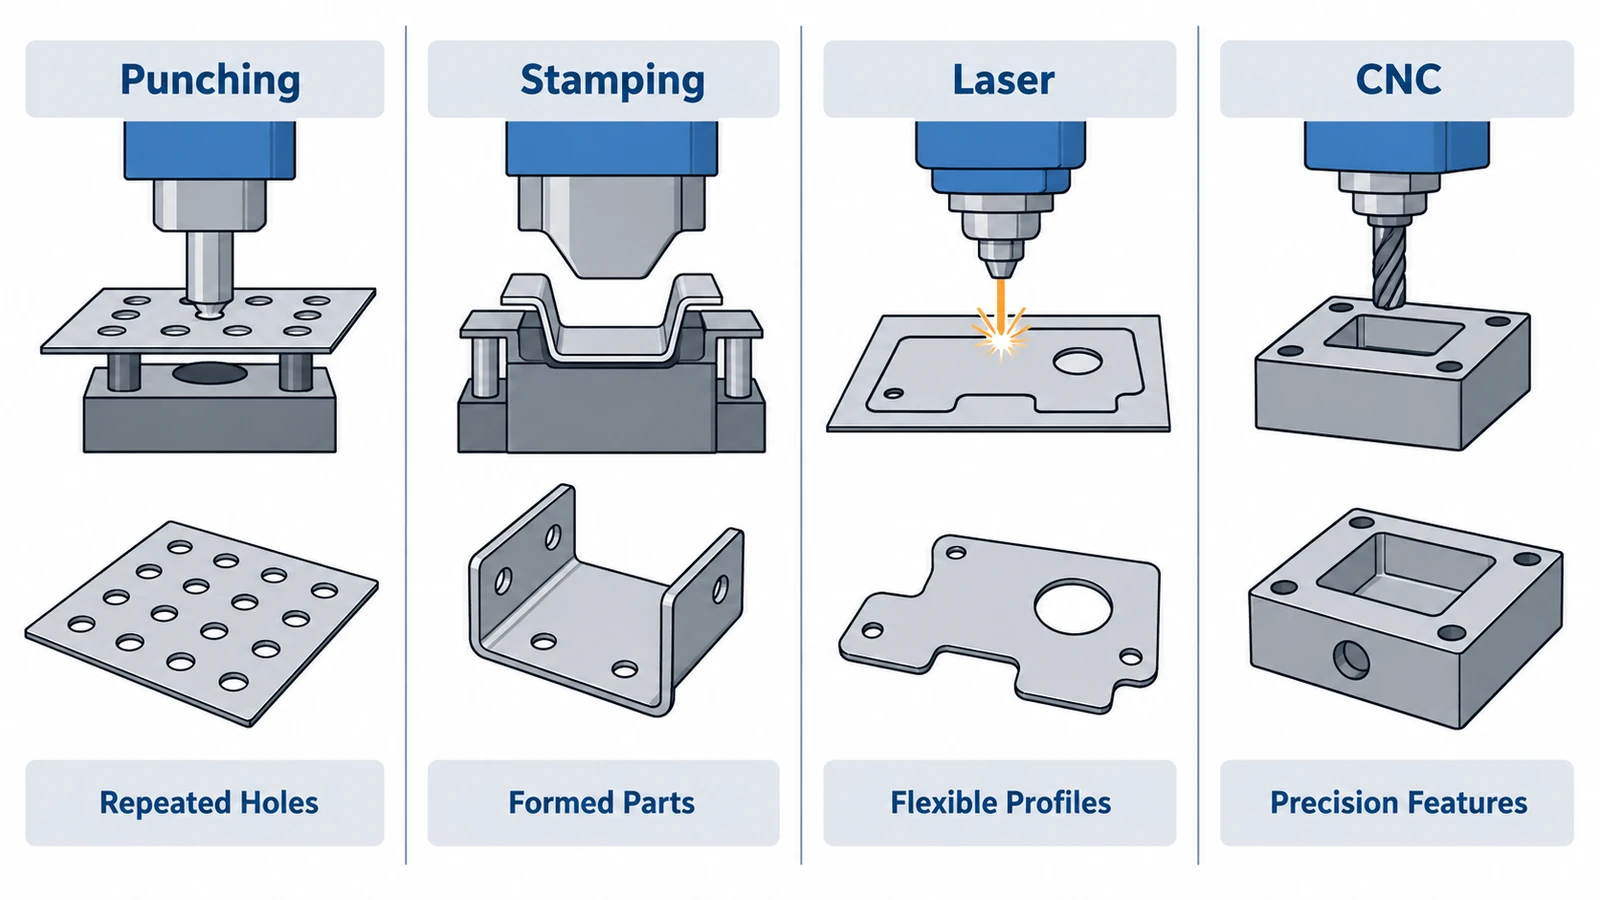
Punching vs Stamping vs Laser Cutting vs CNC Machining
Punching and stamping are not always the best options.
Laser cutting and CNC machining may be more suitable depending on geometry, tolerance, and production quantity.
| Process | Best For | Tooling Cost | Typical Volume | Geometry |
|---|---|---|---|---|
| CNC Punching | Repeated holes, slots, louvers | Low–Medium | Low–High | Mostly flat sheet |
| Stamping | Repetitive formed sheet parts | High | Medium–Very High | Formed sheet |
| Laser Cutting | Flexible profiles and frequent design changes | Very Low | Prototype–Medium | 2D sheet |
| CNC Machining | Precision features and complex geometry | Low | Prototype–Medium | Complex 3D |
When Laser Cutting Is Better
Laser cutting is often more suitable when:
- Production volume is low
- Designs change frequently
- Complex external contours are required
- No suitable punch tooling exists
Because no dedicated cutting tool is required, laser cutting is especially useful during prototyping and early product development.
When Punching Is Better
Punching is often more efficient for:
- Repeated holes
- Slots
- Louvers
- Knockouts
- Perforation patterns
- Extruded holes
Once the appropriate tooling is available, these features can be produced very quickly.
When CNC Machining Is Better
CNC machining is more suitable when a component requires:
- Tight-tolerance bores
- Threaded holes
- Counterbores
- Pockets
- Precision datum surfaces
- Complex 3D features
In some components, punching or stamping produces the basic sheet-metal shape, while CNC machining is used afterward for critical precision features.
Can Punching and Stamping Be Used Together?
Yes.
Punching is often part of a stamping sequence.
A progressive die may perform operations such as:
Punch → Blank → Bend → Form → Cut Off
This is why the terms sometimes overlap.
Punching describes a specific cutting action, while stamping describes the broader process that may combine cutting and forming operations.
Common DFM Issues in Punching and Stamping
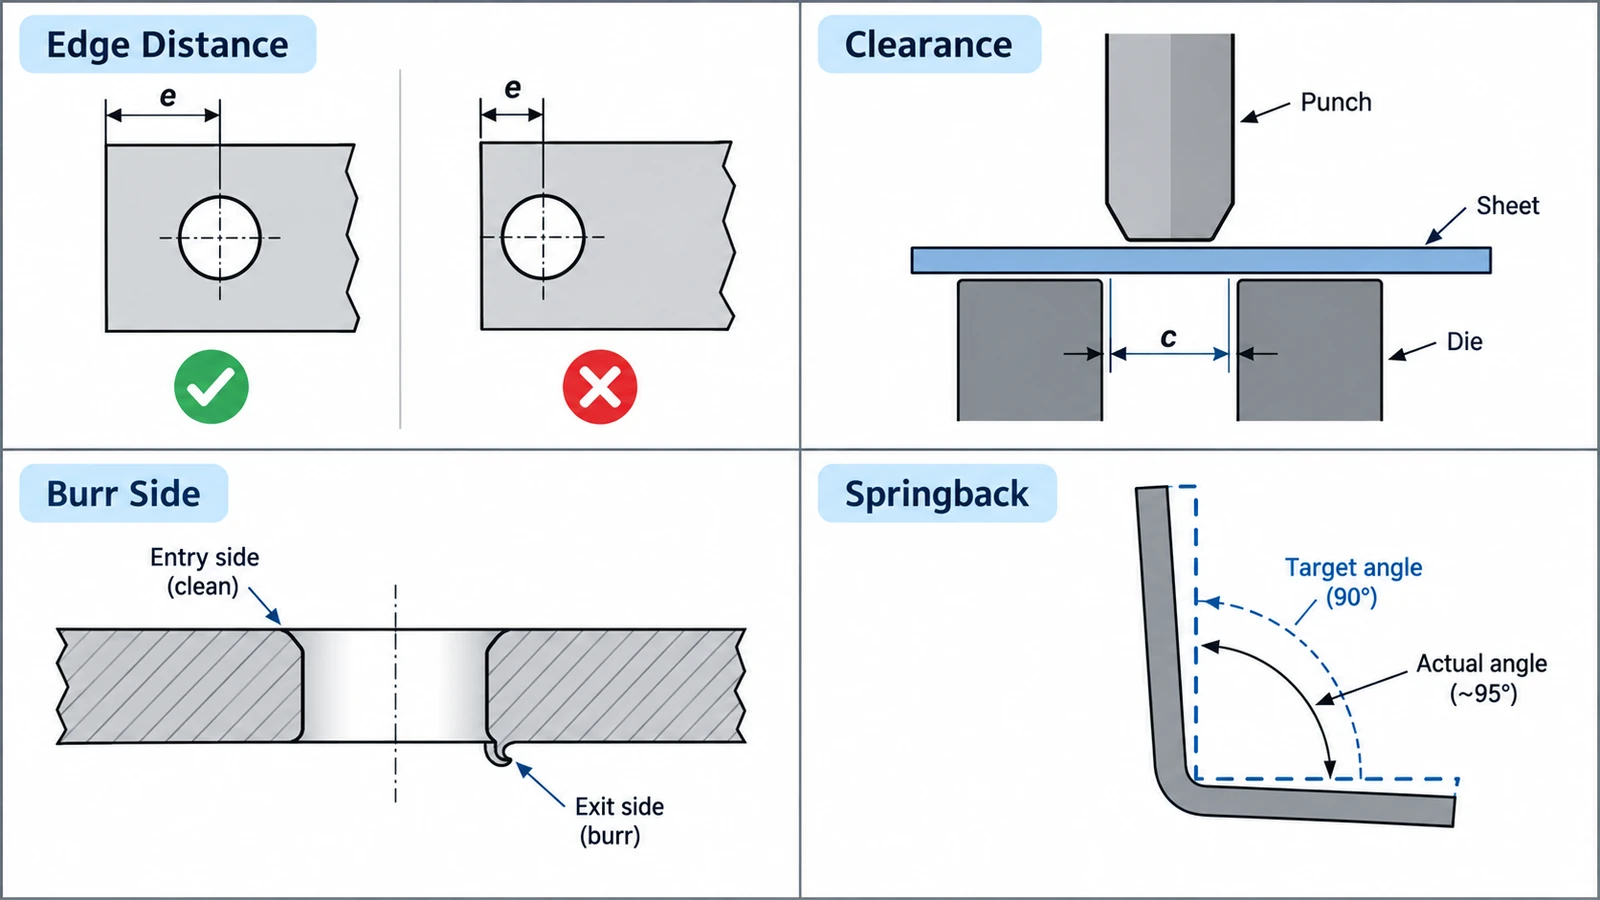
Hole Size and Edge Distance
Very small holes or holes placed too close to an edge can cause distortion or tearing.
Minimum practical dimensions depend on sheet thickness, material strength, tool diameter, and part geometry.Punch-to-Die Clearance
Correct clearance between the punch and die is essential.
Too little clearance increases cutting force and tool wear, while too much clearance can increase burrs and reduce edge quality.
Burr Direction
Punching normally creates different edge conditions on the entry and exit sides of the sheet.
The burr side should therefore be considered when the part has cosmetic, sealing, or assembly requirements.
Springback
Formed sheet metal tends to recover slightly after the forming force is removed.
This springback must be considered when designing bends and stamped features, especially with higher-strength materials.
How to Choose the Right Process
| Your Part Requires | Recommended Process |
|---|---|
| Many repetitive holes | Punching |
| Slots and perforations | Punching |
| Louvers and knockouts | Punching |
| Frequent design changes | Punching or laser cutting |
| Complex low-volume sheet profiles | Laser cutting |
| Multiple formed features | Stamping |
| High-volume formed parts | Stamping |
| Deep-drawn geometry | Stamping |
| Threads, bores, and pockets | CNC machining |
| Tight-tolerance 3D features | CNC machining |
| Prototype before production tooling | Laser cutting or CNC machining |
Punching is usually the better option for flexible sheet-metal parts with repeated holes and cutouts.
Stamping is more attractive when the geometry is stable, forming is required, and production volume is high enough to justify dedicated tooling.
For parts that also require precision bores, threads, pockets, or critical datum surfaces, CNC machining can be used as a secondary operation or as an alternative during prototyping and low-volume production.
Final Thoughts
Metal punching is mainly used to create holes and cutouts, while stamping covers a wider range of cutting and forming operations.
Punching offers greater flexibility and lower initial tooling requirements. Stamping requires more tooling investment but becomes highly efficient for stable, high-volume production.
The best choice depends on geometry, quantity, tolerance, tooling budget, and how mature the design is.
YuanYi provides CNC machining for prototypes, secondary machining, and low-volume precision components. If your part combines sheet-metal geometry with tight-tolerance machined features, send us your drawing or 3D model for DFM review.



